


Leave Your Message


China factory direct auxiliaries designed to optimize automotive-grade pigment dispersion and UV resistance on concrete surfaces.
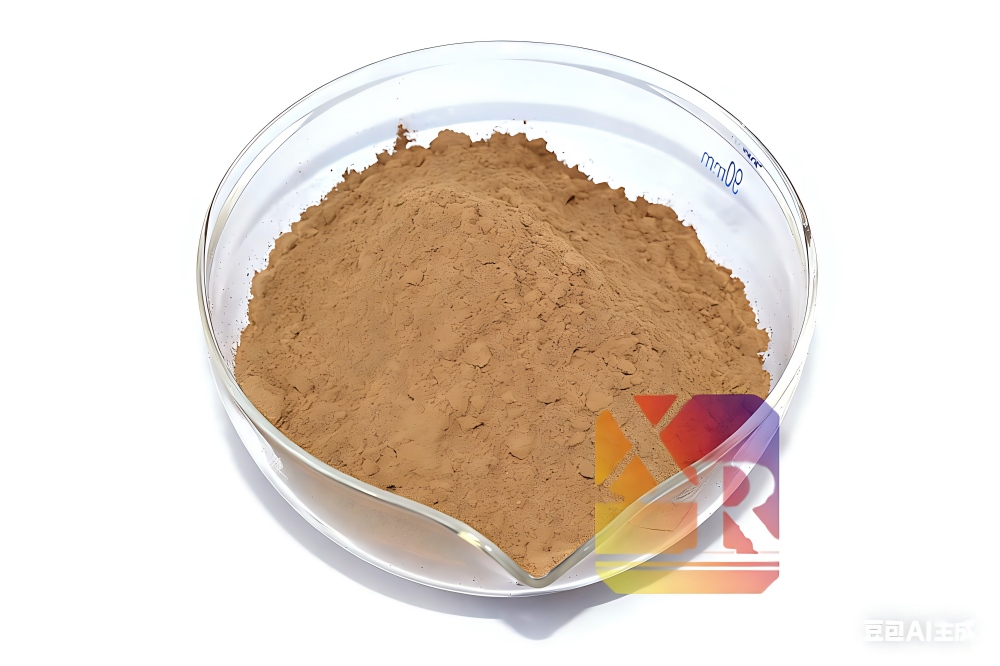
High-quality intermediates optimized for synthesizing weather-stable Azo and Anthraquinone pigments suited for heavy-duty applications.
Engineered intermediates from leading Chinese suppliers to produce vibrant, long-lasting colors for exterior architectural concrete.
Direct from factory solutions that significantly improve film adhesion, color retention, and chemical resistance of concrete stains.
Historically, coloring concrete was a straightforward, almost rudimentary process. Builders relied almost exclusively on natural or synthetic iron oxides to produce muted earth tones—reds, browns, yellows, and blacks. While functional, these traditional colorants lacked the brilliance, depth, and durability required for modern architectural masterpieces and high-wear industrial zones. Today, a revolutionary cross-industry trend is taking center stage: the adaptation of auto paint pigment for adding color to concrete surfaces.
Automotive paint pigments are engineered to withstand the absolute harshest environmental conditions. From blistering UV exposure and acid rain to rapid temperature fluctuations and abrasive physical impacts, these pigments must retain their color integrity for decades. By integrating automotive-grade pigment chemistry—such as advanced Azo and Anthraquinone structures—with specialized concrete carrier systems and multifunctional paint auxiliaries, manufacturers are unlocking a new spectrum of possibilities for concrete surfaces.
"The fusion of automotive pigment technology with modern concrete chemistry represents a monumental leap forward, transitioning concrete from a basic structural element into a vibrant, high-performance design medium."
In the contemporary commercial design landscape, concrete is no longer hidden behind carpets or gypsum boards. Polished concrete floors, precast concrete wall panels, and decorative concrete facades have become the materials of choice for corporate headquarters, luxury retail outlets, museum galleries, and upscale residential developments.
The commercial demand for high-end aesthetics has exposed the limitations of traditional concrete stains. Designers now demand vibrant blues, deep greens, metallic finishes, and even pearlescent effects—colors that are notoriously difficult to stabilize in concrete's highly alkaline environment. Automotive pigments, backed by advanced chemical structures and optimized with multifunctional paint auxiliaries, provide the chemical resilience needed to survive the hydration process of Portland cement and maintain their vibrancy under intense foot traffic and environmental exposure.
Automotive pigments feature unparalleled resistance to solar degradation, ensuring concrete colors do not fade over decades of outdoor exposure.
Formulated to withstand the extreme pH levels of concrete without chemical breakdown or color shifting.
Enables metallic, pearlescent, and high-chroma colors that were previously impossible to achieve on concrete.
Modern skyscraper facades and corporate headquarters utilize precast concrete panels to achieve sleek, monolithic designs. By incorporating automotive-grade organic pigments (such as phthalocyanines and anthraquinones) into the concrete mix, manufacturers can produce panels with striking, non-fading colors. When treated with premium paint auxiliaries, these pigments distribute uniformly, preventing color splotchiness and ensuring consistent coloration across massive surface areas.
Automotive dealerships, luxury retail boutiques, and high-traffic public spaces demand flooring that is both durable and visually arresting. Applying automotive-grade pigment systems via epoxy or polyurethane concrete overlays allows designers to create metallic, high-gloss concrete surfaces that mimic the deep, liquid-like finish of a luxury vehicle. These systems resist tire marks, chemical spills, and heavy foot traffic while maintaining their brilliant sheen.
Public plazas, skate parks, retaining walls, and acoustic barriers are constantly subjected to weathering and vandalism. Utilizing concrete colored with automotive-grade pigments ensures that these structures remain visually appealing over their lifespan. Furthermore, the integration of advanced coating auxiliaries makes these colored concrete surfaces easier to clean and resistant to graffiti removal chemicals.
As the construction and coatings industries move toward sustainability and smart technology, the role of auto paint pigments in concrete is evolving rapidly.
Nanotechnology Integration: Nano-dispersed pigments are being developed to allow deeper penetration into the concrete matrix, creating a more permanent bond and richer color saturation. This prevents the pigment from washing out or wearing off over time.
Cool Pigment Technology: Adapting infrared-reflective automotive pigments to concrete surfaces helps mitigate the urban heat island effect. These pigments reflect solar radiation, keeping concrete pavements and building envelopes cooler, thereby reducing energy consumption in urban areas.
Eco-Friendly Formulations: The shift toward water-based automotive paint systems has spurred the development of zero-VOC, water-compatible pigment dispersions for concrete. This ensures compliance with strict environmental regulations like LEED and green building certifications without sacrificing performance.
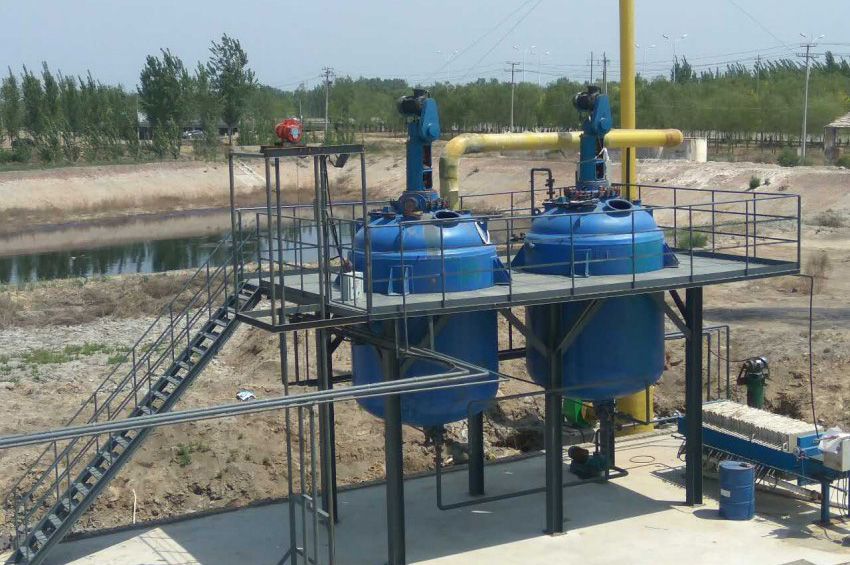
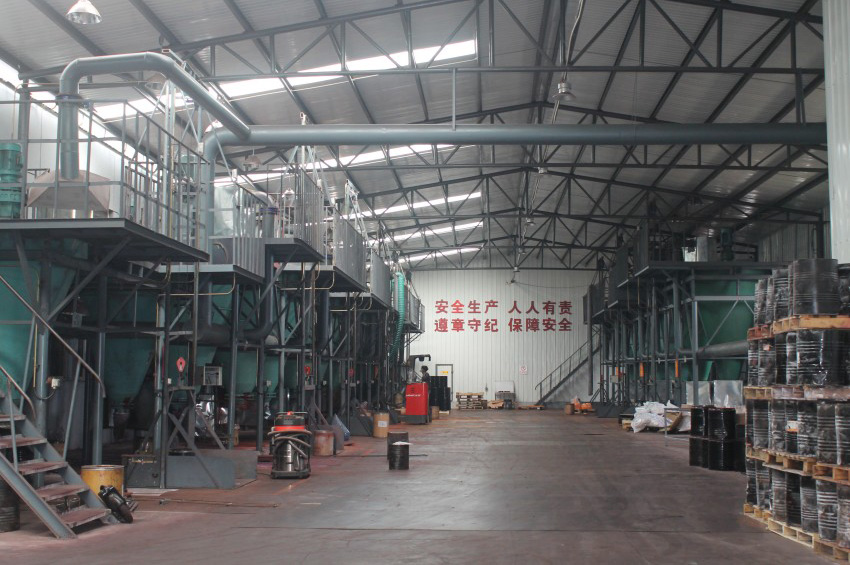
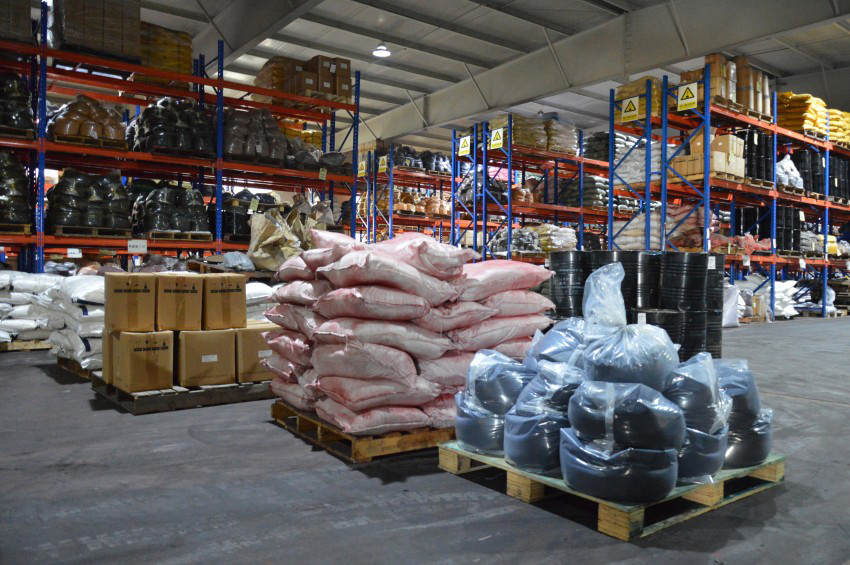
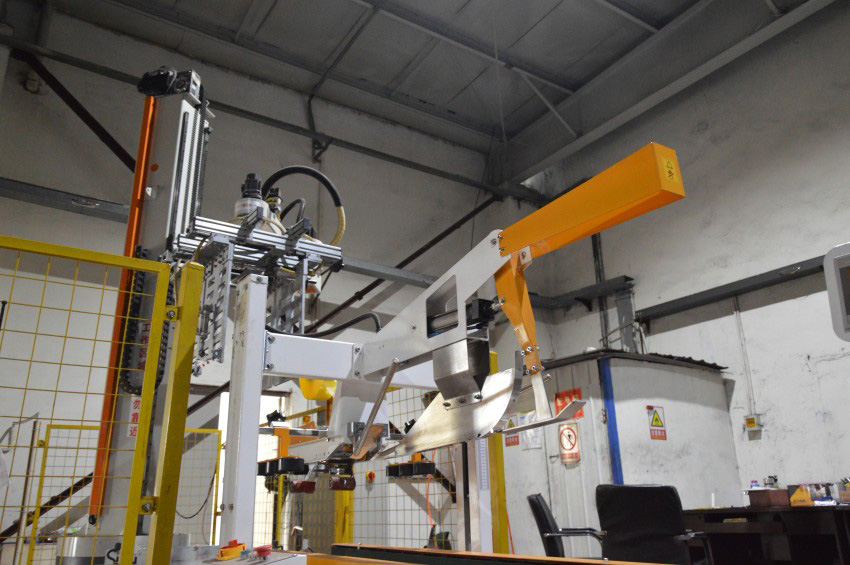
Tianjin Xiangrui Dyestuff Co., Ltd., together with its subsidiary Tianjin Xiangrui International Trading Co., Ltd., was established in 1998 and 2021 respectively. The company is located in Dasi Industrial Park, Xiqing Economic Development Area, Tianjin, China, and currently employs several hundred staff members.
Xiangrui specializes in the manufacture and supply of a wide range of different dyes, pigments, chemical auxiliaries, and intermediates, which are widely applied in industries such as textiles, papermaking, leather, coatings, inks, plastics, rubber, aluminum, cosmetics, and agriculture.
With an annual production capacity of approximately 18,000 tons, Xiangrui is able to provide stable and reliable supply to customers worldwide.
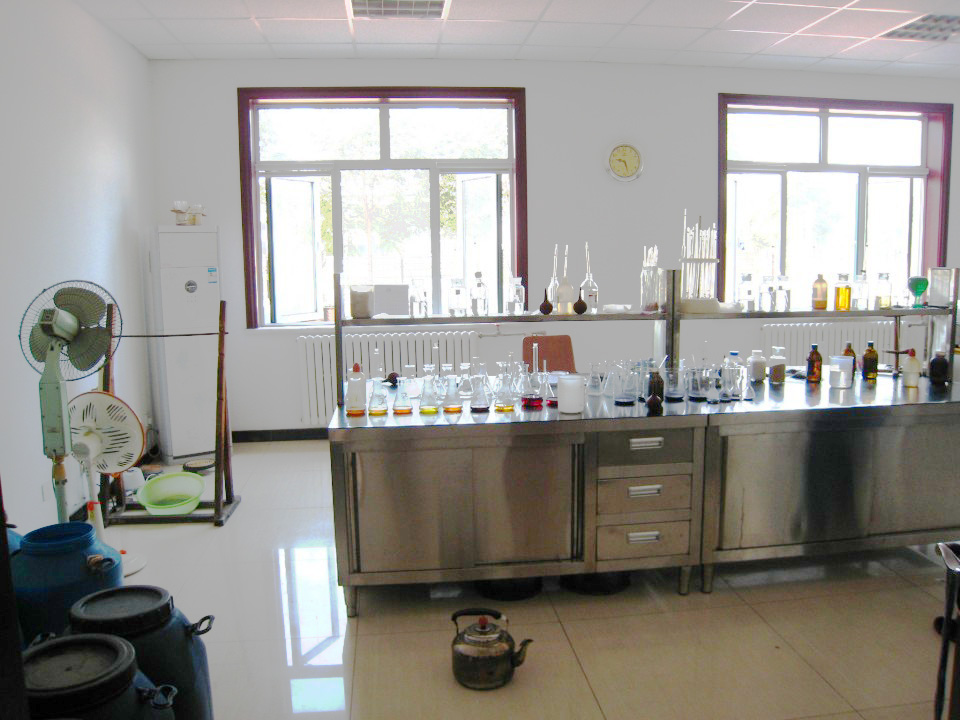
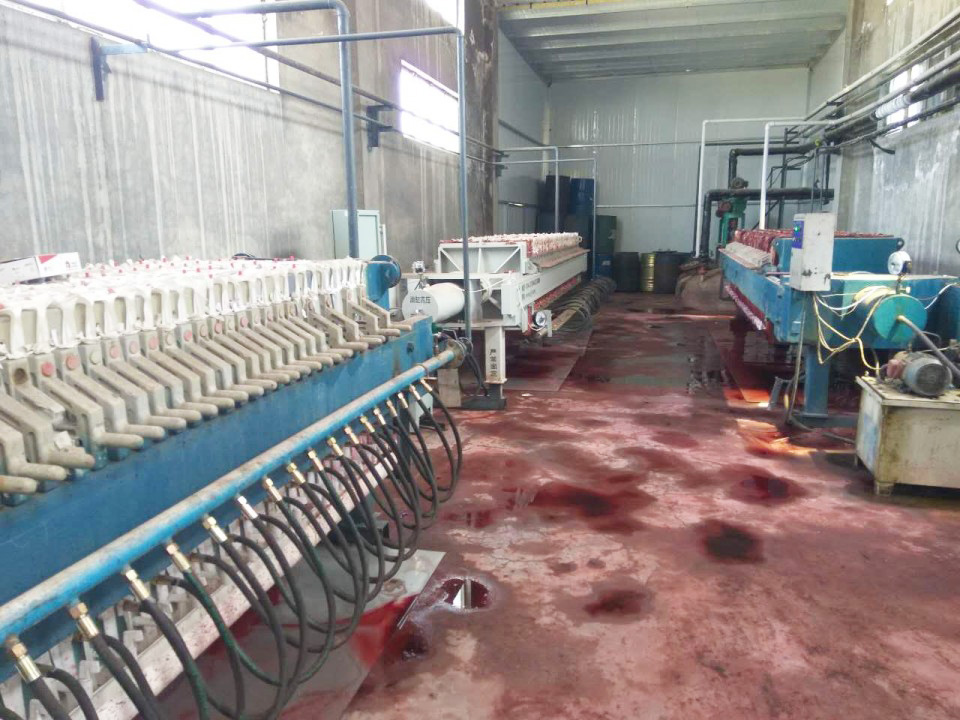
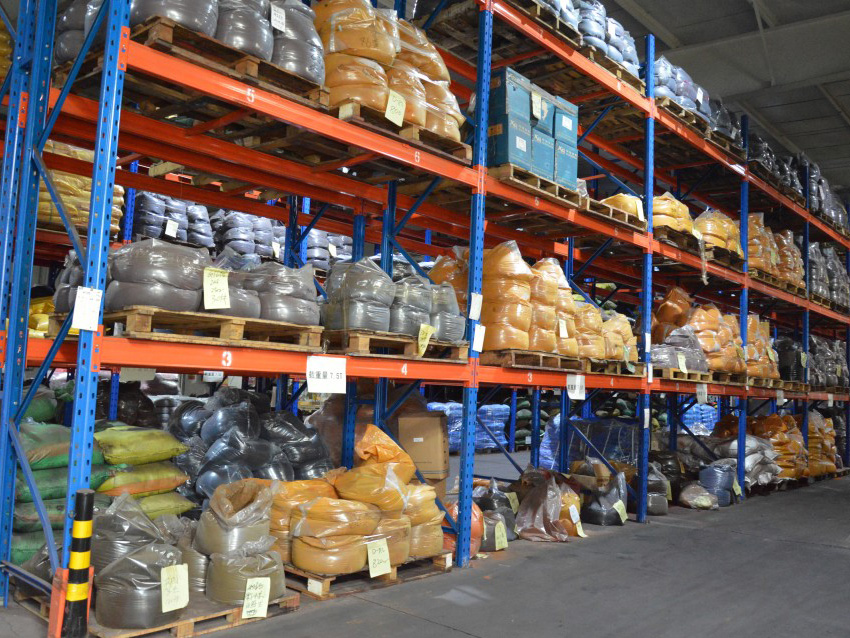
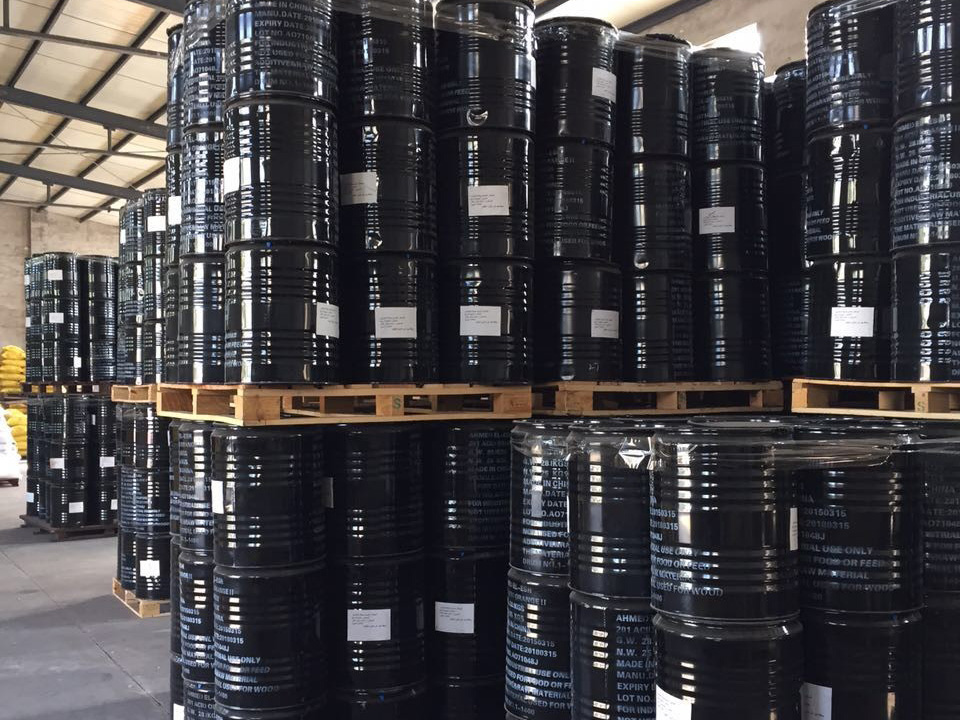
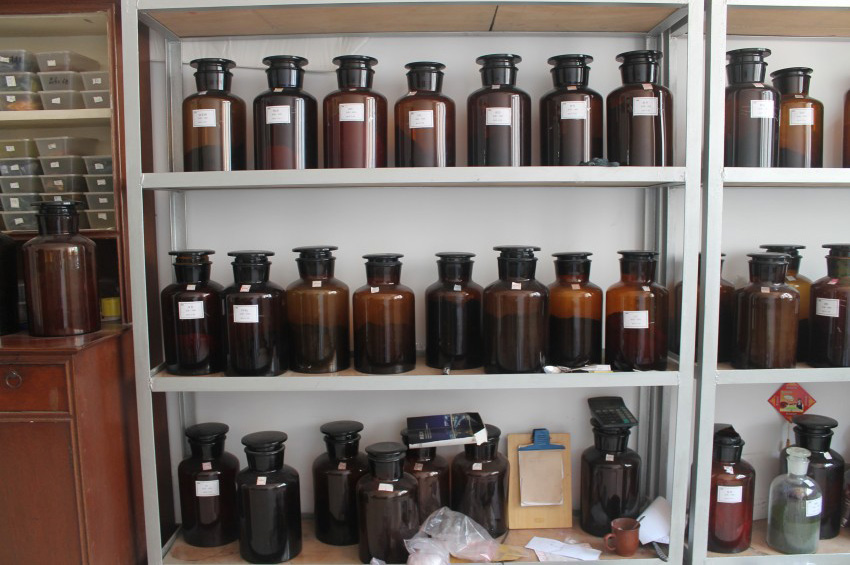
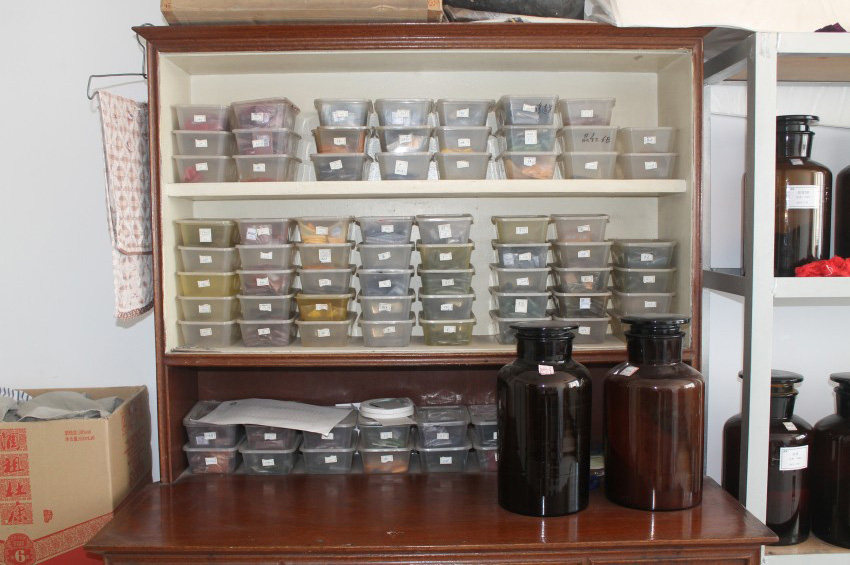
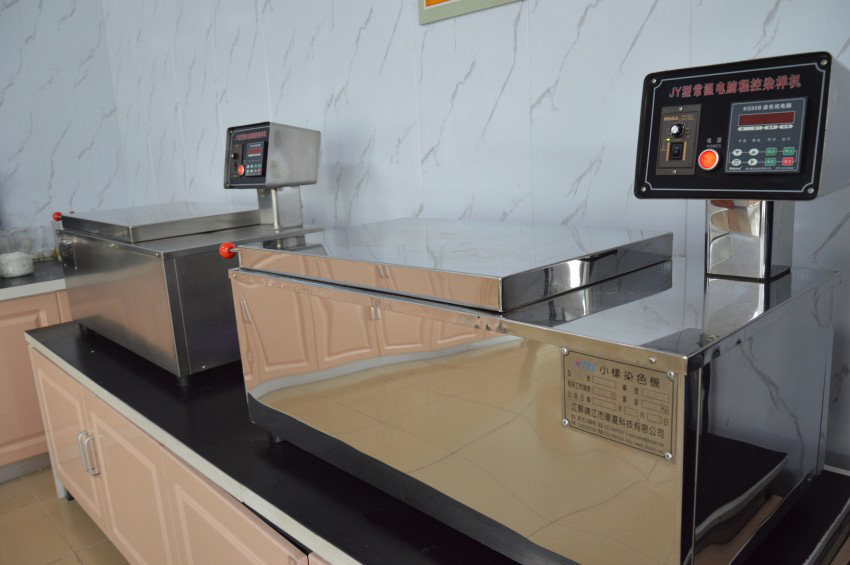
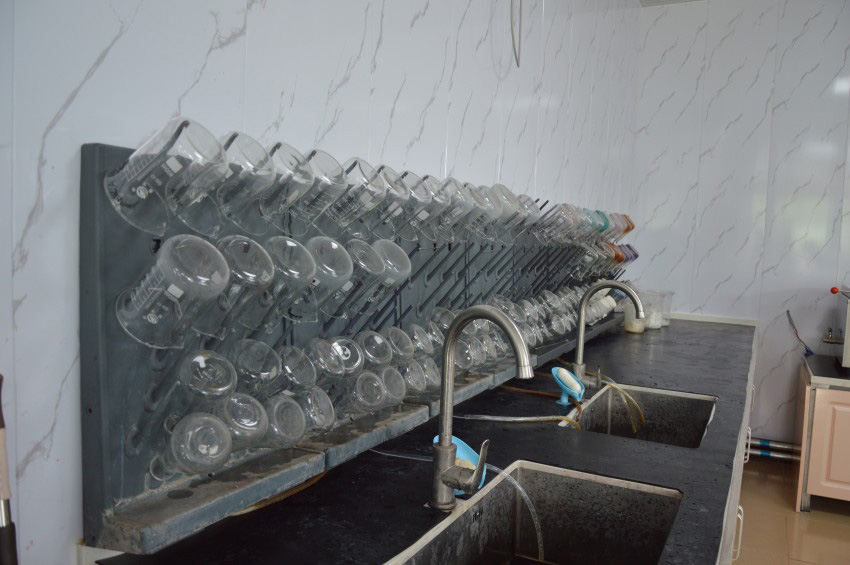
After years of continuous development, Xiangrui has established a fully integrated operation covering research and development, production, sales, and after-sales technical support. Supported by advanced manufacturing facilities, experienced R&D professionals, and a strict quality control system. We are committed to delivering products with consistent quality and performance.
Owing to superior product quality, professional service, and competitive pricing, Xiangrui has grown into one of the leading dyestuff manufacturers in North China, with products well recognized both in the domestic market and in overseas markets.
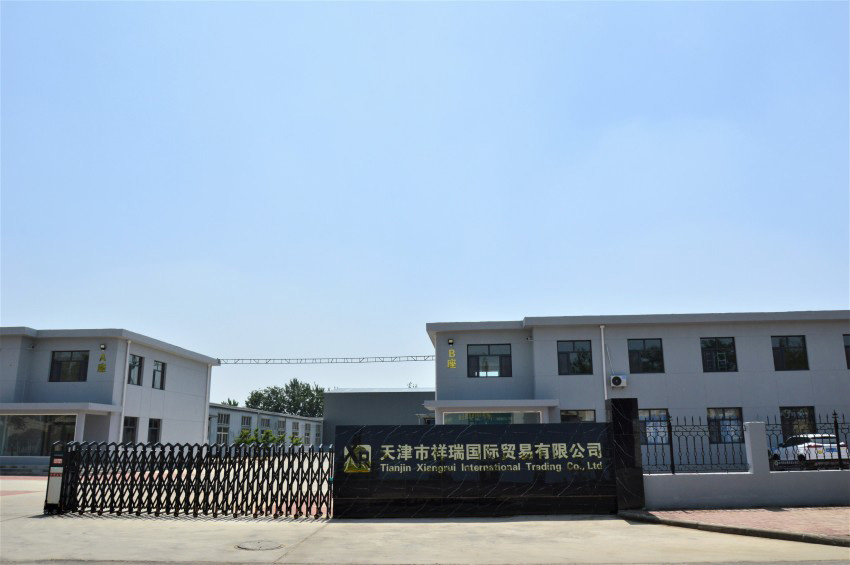
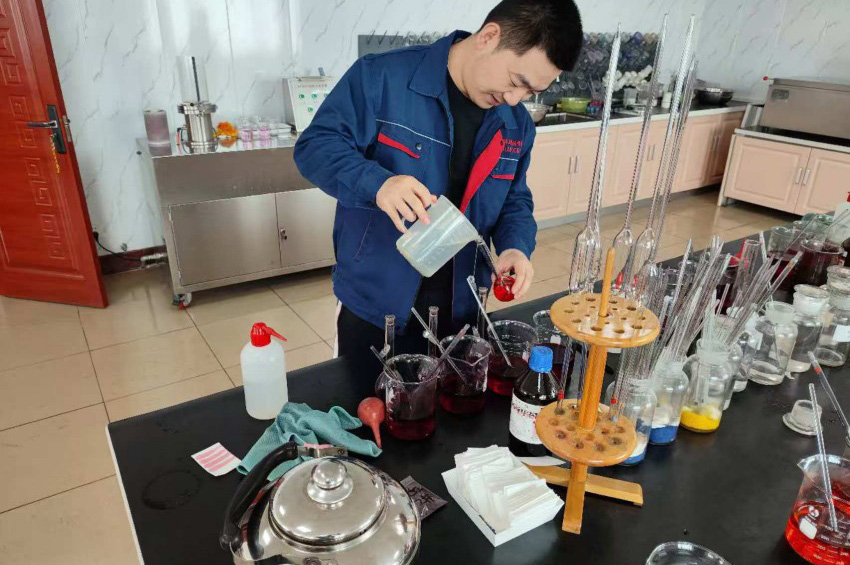
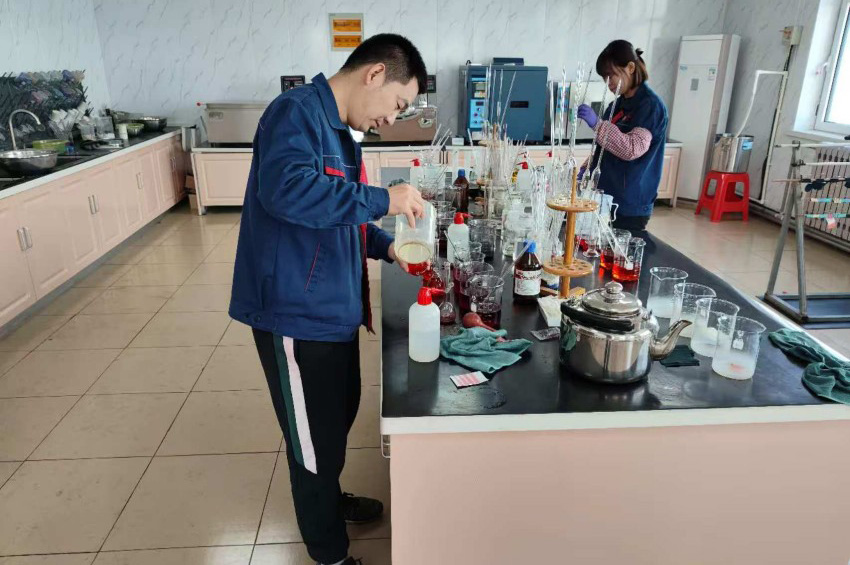
Our core values guide every step we take towards technological innovation and customer satisfaction.
Continuously evaluating gaps from multiple perspectives in order to achieve our goals and improve standardization and management efficiency.
Focusing on strengthening the company’s core capabilities, team development, and professional expertise while maintaining an international vision.
Committed to creating long-term value for customers, employees, partners, and society as a whole.
Pursuing continuous innovation and improvement to enhance product quality and to meet the evolving demands of future markets.
With an elite international sales team, experienced technical experts, and a professional quality management system, Xiangrui enjoys a solid reputation among global customers. We strictly implement internal enterprise standards and continuously optimize our management system to meet international market requirements.
China factory direct auxiliaries designed to optimize automotive-grade pigment dispersion and UV resistance on concrete surfaces.
High-quality intermediates optimized for synthesizing weather-stable Azo and Anthraquinone pigments suited for heavy-duty applications.
Engineered intermediates from leading Chinese suppliers to produce vibrant, long-lasting colors for exterior architectural concrete.
Direct from factory solutions that significantly improve film adhesion, color retention, and chemical resistance of concrete stains.
High-purity chemical intermediates essential for formulating automotive-grade pigments used in concrete coloring systems.
Advanced chemical solutions providing enhanced scratch resistance and leveling properties for concrete sealers and coatings.
Engineered to protect colored concrete surfaces from water intrusion, freeze-thaw damage, and color fading.
High-grade organic intermediates synthesized for the production of vibrant, heat-stable pigments for industrial concrete stains.