Leave Your Message


The evolution of architectural and industrial design has brought concrete out of the shadows of mere structural utility and into the spotlight of aesthetic and functional brilliance. At the heart of this transformation is Concrete Dye Powder, a revolutionary coloring agent that, when combined with advanced chemical auxiliaries, delivers unparalleled dyeing performance.
Unlike traditional acid stains that rely on unpredictable chemical reactions with the concrete's free lime, concrete dye powders offer a more controlled, vibrant, and consistent coloring solution. By leveraging cutting-edge auxiliaries—such as penetration enhancers, UV stabilizers, and binding agents—the performance of concrete dye powder is significantly amplified. This synergy ensures deep substrate penetration, extraordinary color fastness, and long-lasting durability, even in the most demanding environments.
The global concrete floor coatings and dyes market has witnessed exponential growth over the past decade. This surge is predominantly driven by rapid urbanization, massive industrialization, and a growing architectural emphasis on sustainable, low-maintenance, and visually appealing flooring solutions.
In today's highly competitive commercial landscape, aesthetics play a crucial role in shaping brand identity and enhancing customer experience. Concrete dye powders have rapidly become the go-to choice for architects, interior designers, and facility managers seeking to transform dull, gray structural slabs into visually stunning surfaces. The market is currently experiencing a massive paradigm shift towards eco-friendly and low-VOC (Volatile Organic Compounds) products. This shift is prompting manufacturers to develop highly refined dye powders and specialized auxiliaries that meet stringent global environmental regulations without compromising on the vividness or longevity of the coloring performance. The integration of high-performance auxiliaries has opened up entirely new avenues for concrete dyes, allowing them to be utilized in environments previously deemed too harsh, chemically aggressive, or physically demanding for colored concrete.
The construction industry's widespread adoption of polished concrete is a primary driver for the increased demand for premium concrete dye powders. Polished concrete floors, renowned for their high reflectivity, exceptional durability, and ease of maintenance, require coloring solutions that can withstand rigorous mechanical grinding and polishing processes. Here, chemical auxiliaries play a pivotal role. Densifiers and hardeners, acting as specialized interactive auxiliaries, react intelligently with the concrete matrix to create a significantly denser surface, effectively locking in the dye powder particles and preventing premature wear or fading. Furthermore, the modern infrastructure sector is increasingly utilizing vibrantly colored concrete for essential safety demarcations, intelligent traffic routing, and urban beautification projects, demanding dyes that offer exceptional UV resistance and extreme weatherability.
The remarkable versatility of concrete dye powder, when precisely enhanced by tailored chemical auxiliaries, allows for its flawless application across a diverse range of scenarios, each presenting its own unique set of physical challenges and aesthetic requirements.
In dynamic retail environments, such as high-end shopping malls, luxury boutiques, and expansive automotive showrooms, the floor is an integral, highly visible part of the interior design strategy. Concrete dye powders offer an incredibly extensive palette of vibrant, translucent colors, enabling designers to create custom intricate patterns, embed corporate logos, and establish clear spatial delineations. Auxiliaries such as advanced leveling agents and deep-penetration enhancers ensure a perfectly even distribution of color across vast square footages, entirely eliminating unsightly mottling, streaking, or lap marks. Additionally, the use of high-gloss, optically clear sealing auxiliaries not only protects the delicate dye from relentless high foot traffic but also dramatically enhances the ambient lighting of the commercial space, subsequently reducing overall energy costs.
Industrial settings demand uncompromising flooring solutions that can endure extreme mechanical stress, including continuous heavy forklift traffic, corrosive chemical spills, and severe impact shocks. While pure aesthetics might seem secondary in these environments, colored concrete is absolutely vital for occupational safety zoning, clearly defining pedestrian walkways, and prominently marking hazardous operational areas. Concrete dye powders utilized in these rigorous environments are heavily fortified with industrial-grade heavy-duty auxiliaries, such as cross-linking epoxy or advanced polyurethane binders. These auxiliaries provide a highly chemically resistant and virtually impermeable shield over the dyed surface. This engineered synergy ensures that critical safety markings remain highly visible and physically intact, significantly reducing costly maintenance downtime and drastically improving overall workplace safety protocols.
The residential housing sector has seen a massive surge in the creative use of concrete dye powders for both sophisticated interior and resilient exterior applications. Homeowners are increasingly opting for elegantly dyed concrete floors in living rooms, gourmet kitchens, and finished basements as a highly hypoallergenic, thermally efficient, and easy-to-clean alternative to traditional carpets or hardwood flooring. For exterior residential applications like sprawling patios, luxurious pool decks, and sweeping driveways, the primary technical challenge lies in combating aggressive color fading caused by relentless sun exposure. By meticulously incorporating advanced UV-stabilizing auxiliaries into the dye formulation, professional contractors can confidently guarantee that the rich, earthy tones or vibrant contemporary hues of the outdoor concrete remain absolutely pristine for years, successfully resisting the degrading effects of ultraviolet radiation and harsh seasonal weather conditions.
Expansive public squares, municipal parks, and bustling urban transit hubs utilize colored concrete to significantly enhance the civic landscape and intuitively guide heavy pedestrian traffic. These large-scale municipal projects require concrete dye powders that can be applied highly efficiently and perfectly consistently over incredibly vast areas. Specialized retarding auxiliaries are frequently utilized to strategically extend the working time of the dye solution, allowing application crews to achieve a flawless, seamless finish without any overlapping marks. Additionally, microscopic anti-slip auxiliaries can be seamlessly integrated into the final protective sealing coat, ensuring that the vibrantly dyed concrete surfaces remain completely safe and compliant for public use, even in exceptionally wet or freezing conditions.
Reduces surface tension for deep, permanent capillary network penetration.
Sacrificial molecular shields preventing photodegradation and color fading.
Cross-linking resins that lock dye particles and seal concrete pores.
Nano-sized particles for extreme color saturation and self-cleaning traits.
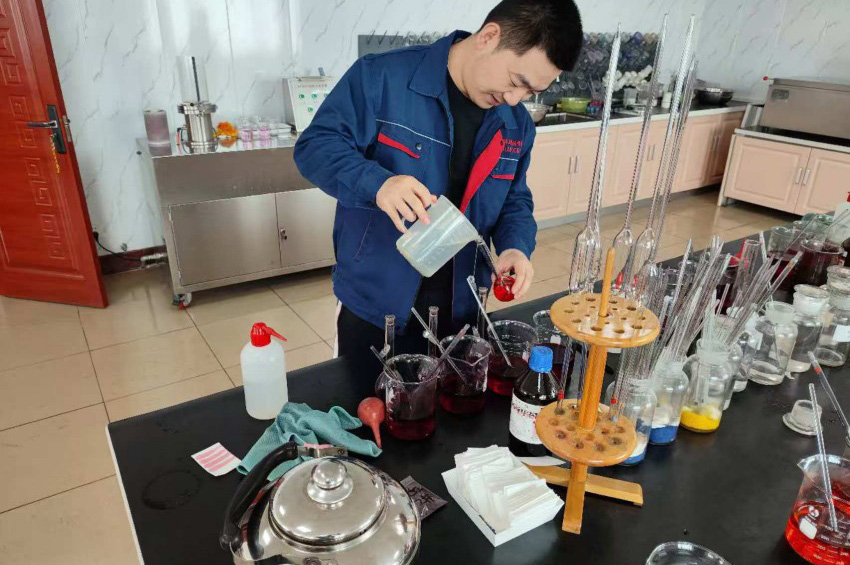
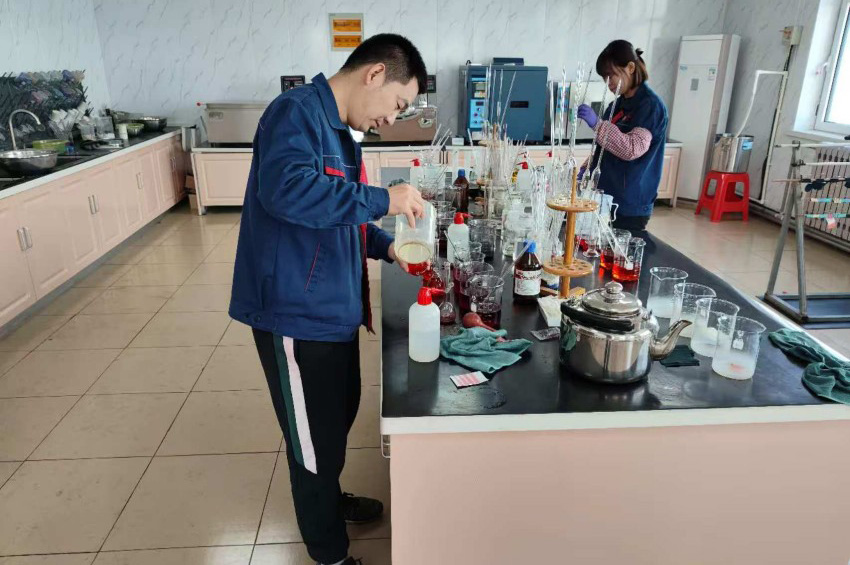
Chemical auxiliaries are the unsung heroes in the highly technical realm of concrete dyeing. These sophisticated chemical additives are meticulously formulated by advanced R&D laboratories to interact seamlessly with the dry dye powder and the rigid concrete matrix, proactively addressing specific physical performance limitations and exponentially elevating the overall quality, durability, and aesthetic appeal of the final architectural finish.
Concrete, despite its solid appearance, is an inherently porous material; however, its surface density can vary wildly depending on the finishing techniques used during pouring. Penetration enhancers, often intelligently formulated from cutting-edge synthetic surfactants and specialized wetting agents, drastically reduce the surface tension of the liquid dye solution. This critical chemical alteration allows the dye powder, once completely dissolved in an appropriate carrier solvent or distilled water, to penetrate significantly deeper into the concrete's microscopic capillary network. Deep penetration is absolutely critical for long-term success; it ensures that the vibrant color is not merely sitting precariously on the topmost surface where it can be easily scratched, abraded, or worn away by foot traffic, but is fundamentally embedded within the upper structural layer of the concrete slab itself.
One of the primary historical challenges associated with organic concrete dye powders is their inherent susceptibility to rapid photodegradation when continuously exposed to harsh sunlight. UV stabilizers act as an invisible, sacrificial chemical shield, aggressively absorbing or scattering harmful ultraviolet rays before they possess the energy to break down the delicate chromophores within the complex dye molecules. Color fastness agents further complement this by chemically locking the dye at a fundamental molecular level, completely preventing unsightly color bleeding, migrating, or shifting over extended periods. This powerful chemical combination is absolutely essential for any exterior hardscape application or interior architectural spaces featuring large panoramic windows and abundant natural light.
Once the perfectly formulated dye has successfully penetrated the concrete matrix, it must be rigorously protected from external environmental threats. Binding auxiliaries, such as high-grade acrylic, industrial epoxy, or advanced aliphatic urethane resins, are subsequently applied to definitively seal the microscopic pores of the concrete. These intelligent auxiliaries cross-link upon curing to form an incredibly durable, transparent protective film that permanently locks the dye powder safely in place. They provide unparalleled resistance against destructive water ingress, aggressive oil spills, and stubborn chemical stains, while simultaneously enhancing the overall structural integrity of the concrete surface. The specific choice of binding auxiliary dictates the final aesthetic finish—ranging from a subtle, natural matte to a striking, high-gloss reflection—and fundamentally determines the floor's long-term maintenance lifecycle.
The global concrete dyeing industry is currently on the precipice of a massive technological revolution, driven equally by the urgent need for smarter, greener, and vastly more efficient construction materials.
As global environmental awareness reaches unprecedented levels, the construction chemical industry is moving rapidly away from traditional solvent-based dyes that release harmful Volatile Organic Compounds (VOCs) into the atmosphere. The undisputed future lies in highly advanced water-based concrete dye powders and innovative bio-based chemical auxiliaries derived entirely from renewable agricultural resources. These sustainable, next-generation solutions offer the exact same, if not vastly superior, performance characteristics as their legacy solvent-based counterparts, ensuring completely safe application in tightly enclosed commercial spaces and drastically minimizing the overall environmental carbon footprint of large-scale construction projects.
Quantum nanotechnology is making incredibly significant inroads into modern concrete dye formulations. Incredibly small, nano-sized dye particles possess the unique physical ability to penetrate even the absolute densest, most highly polished concrete surfaces with remarkable ease, achieving unprecedented levels of color saturation, clarity, and three-dimensional depth. Furthermore, the integration of smart nano-auxiliaries can successfully impart revolutionary self-cleaning properties to the dyed concrete (often referred to as the biomimetic lotus effect), where water droplets literally roll off the surface, effortlessly picking up dirt, dust, and organic debris along the way. This technological leap drastically reduces the ongoing need for harsh, expensive chemical cleaners and significantly lowers long-term facility maintenance costs.
Achieving a truly flawless, exceptionally long-lasting colored concrete floor requires significantly more than just purchasing high-quality chemical materials; it demands meticulous, professional execution and strict adherence to established industry best practices.
The ultimate success of any high-end concrete dyeing project hinges entirely on proper, uncompromising surface preparation. The target concrete must be immaculately clean, structurally sound, and completely free of any pre-existing coatings, curing compounds, sealers, dirt, or industrial grease. Mechanical profiling, utilizing heavy-duty diamond grinding or aggressive shot blasting equipment, is highly recommended to physically open the concrete's pores and successfully create a highly receptive surface profile. Precision is absolutely key when mixing the concentrated concrete dye powder with its designated liquid carrier and specialized auxiliaries. Applicators must strictly follow the manufacturer's scientifically recommended ratios to ensure perfect optical color consistency and maximum chemical performance. Post-application, allowing adequate, uninterrupted curing time before applying the final protective sealing auxiliaries is absolutely crucial to permanently lock in the vibrant color and guarantee maximum lifecycle durability.
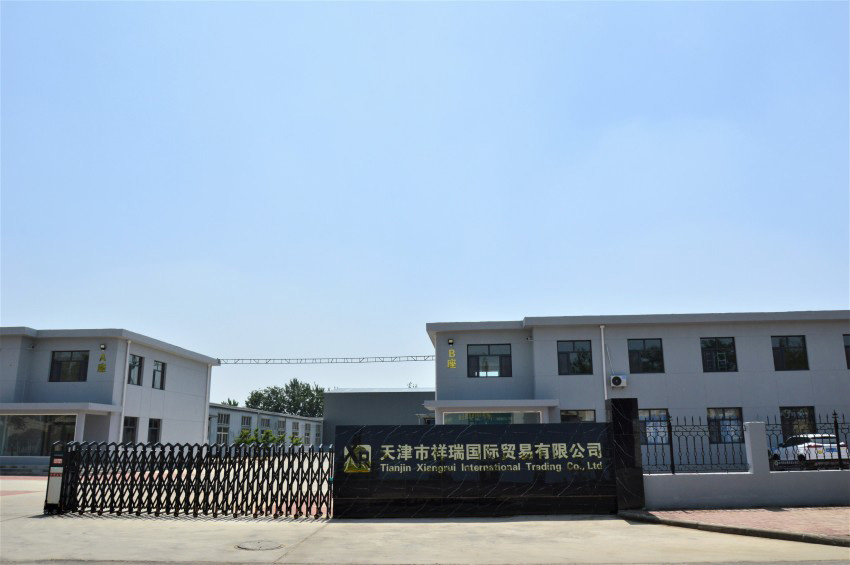
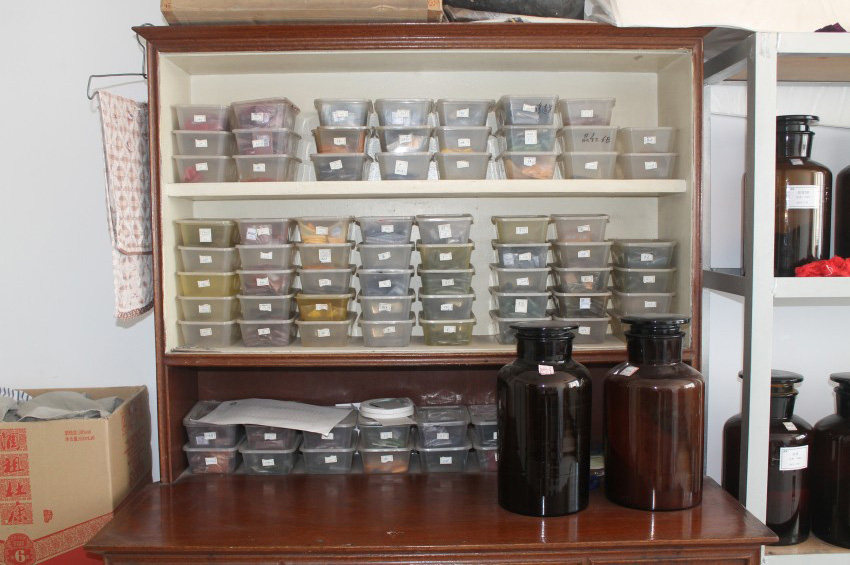
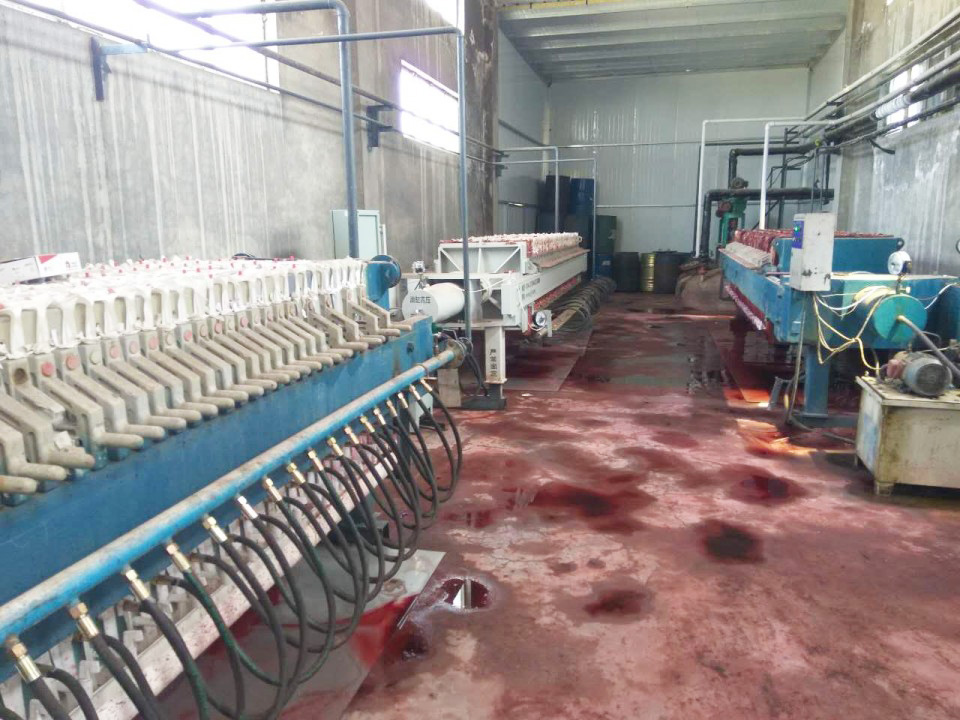
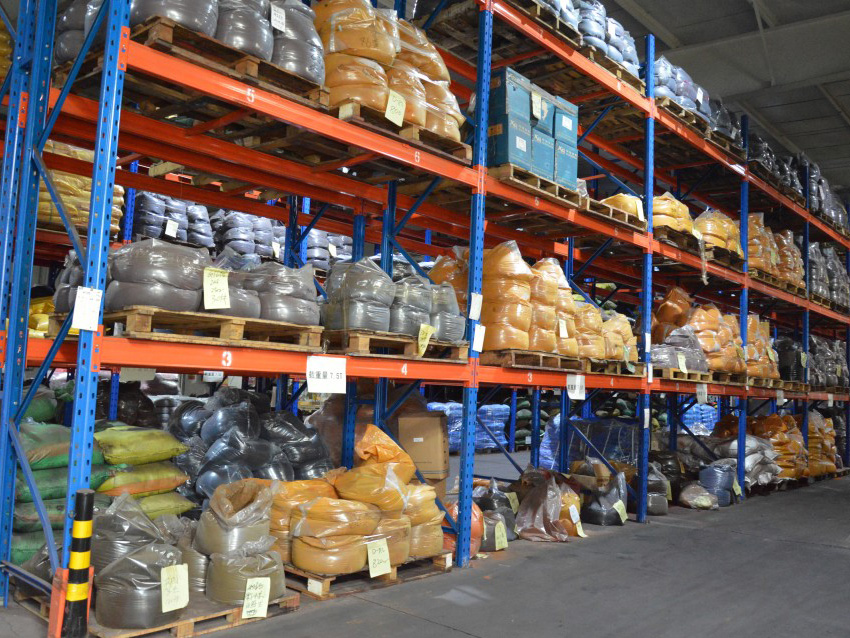
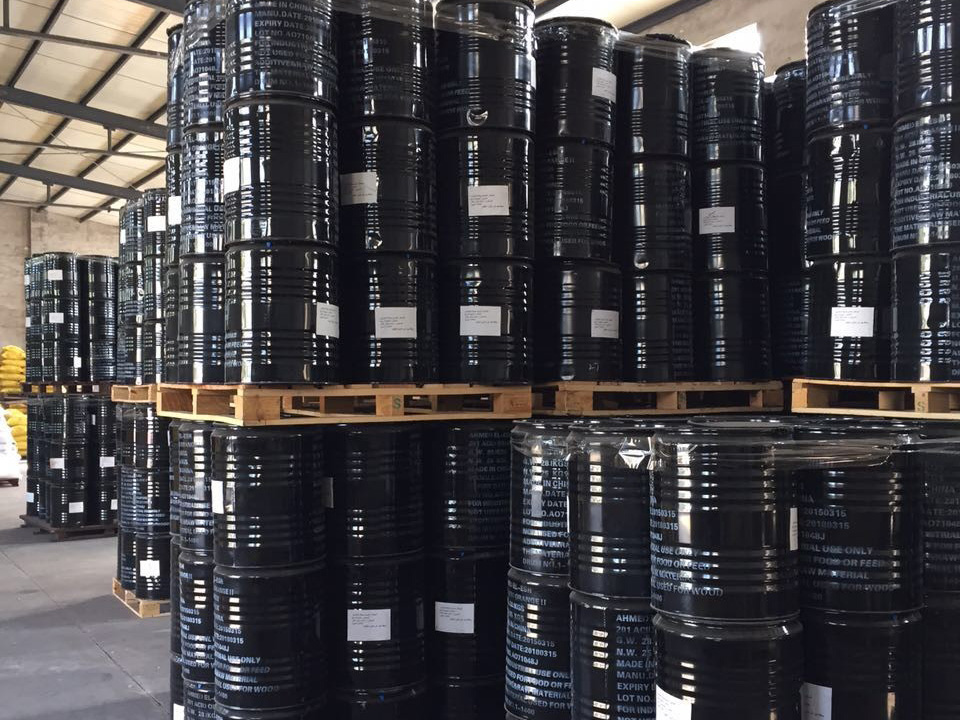
Established in 1998, Tianjin Xiangrui Dyestuff Co., Ltd., together with its subsidiary Tianjin Xiangrui International Trading Co., Ltd. (established in 2021), represents the pinnacle of chemical manufacturing excellence. Located strategically in the Dasi Industrial Park, Xiqing Economic Development Area, Tianjin, China, our company currently employs several hundred dedicated staff members committed to industrial innovation.
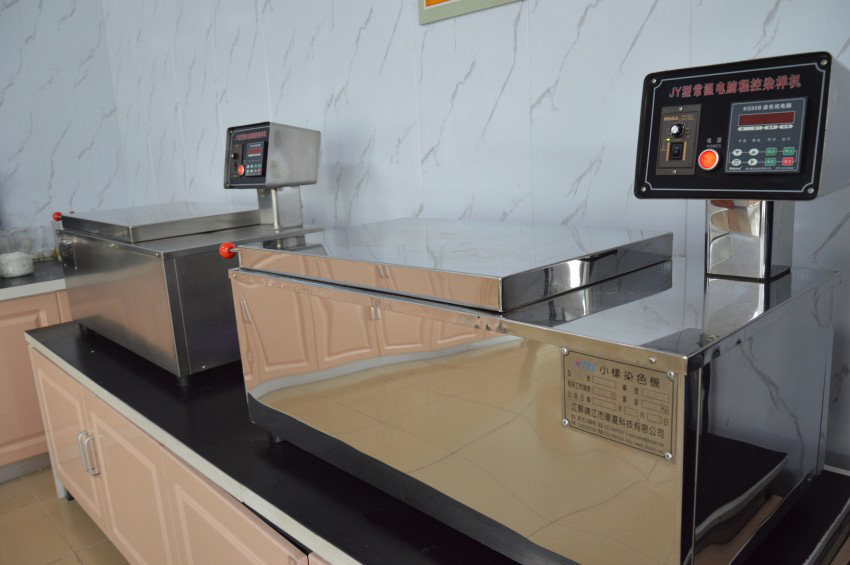
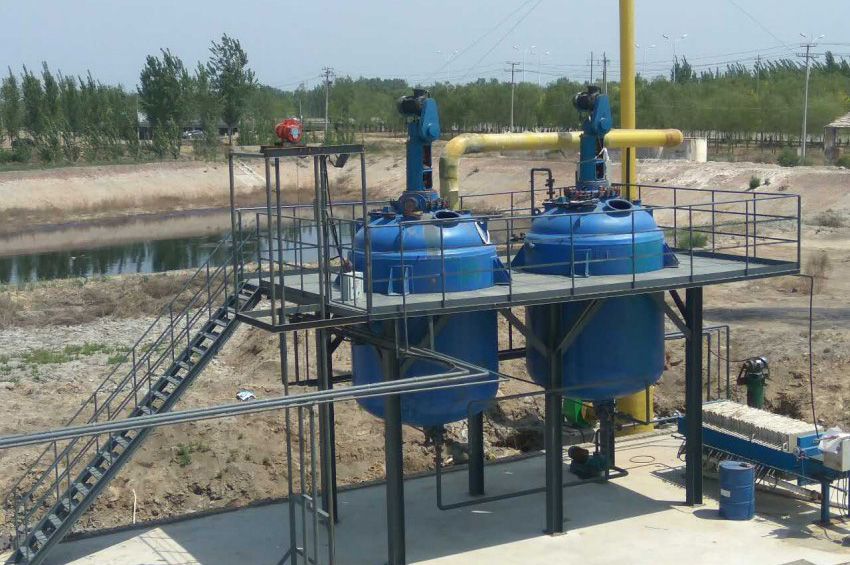
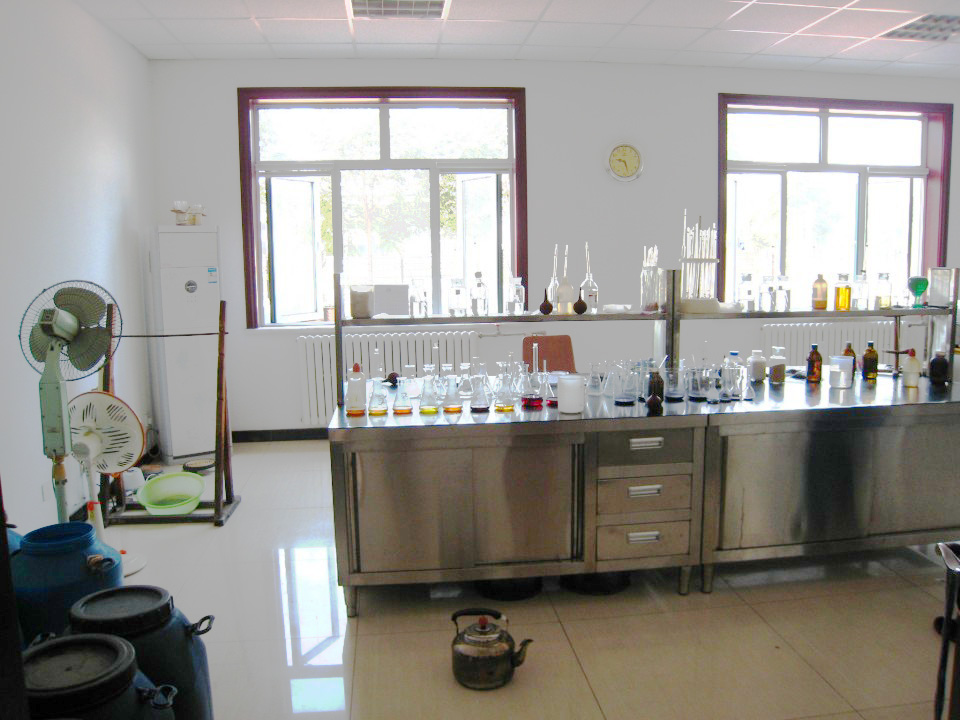
After years of continuous development, Xiangrui has established a fully integrated operation covering research and development, production, sales, and after-sales technical support. Supported by advanced manufacturing facilities, experienced R&D professionals, and a strict quality control system, we are committed to delivering products with consistent quality and performance. Owing to superior product quality, professional service, and competitive pricing, our products are well recognized both in the domestic market and in overseas markets.
Continuously evaluating gaps from multiple perspectives in order to achieve our goals and improve standardization and management efficiency.
Focusing on strengthening the company’s core capabilities, team development, and professional expertise while maintaining an international vision.
Committed to creating long-term value for customers, employees, partners, and society as a whole.
Pursuing continuous innovation and improvement to enhance product quality and to meet the evolving demands of future markets.
With an elite international sales team, experienced technical experts, and a professional quality management system, Xiangrui enjoys a solid reputation among global customers.
We strictly implement internal enterprise standards and continuously optimize our management system to meet international market requirements. All staff of Xiangrui sincerely welcome your visit and cooperation.