Leave Your Message


High-performance disperse dye solutions engineered for superior results in textile dyeing and auxiliary-enhanced applications.
Unlocking the full potential of disperse dyes through the science of chemical auxiliaries in industrial textile dyeing.
Disperse dyes are a class of water-insoluble synthetic dyes primarily used for dyeing hydrophobic fibers such as polyester, acetate, nylon, and other synthetic textiles. Unlike reactive or direct dyes, disperse dyes do not dissolve in water but are instead dispersed as fine particles throughout the dye bath with the help of dispersing agents. Their molecular structure allows them to diffuse into the polymer matrix of synthetic fibers at elevated temperatures, forming a solid solution within the fiber.
The performance of disperse dyes — including color depth, levelness, fastness properties, and reproducibility — is profoundly influenced by the chemical auxiliaries used alongside them. Auxiliaries act as functional enhancers that optimize the dye-fiber interaction, improve bath stability, reduce defects, and increase process efficiency. In modern industrial dyeing, the selection and combination of the right auxiliaries is just as critical as the choice of the dye itself.
Dispersing agents are perhaps the most fundamental auxiliary in disperse dyeing. They prevent dye aggregation in the bath, maintain particle size stability under high-temperature conditions, and ensure uniform dye distribution on the fiber surface. High-quality dispersing agents — such as naphthalene sulfonate condensates and lignosulfonates — significantly improve the migration and leveling of disperse dyes, reducing patchiness and uneven coloration.
Leveling agents control the rate of dye uptake by the fiber, ensuring that dye molecules are evenly distributed throughout the textile substrate. In high-temperature, high-pressure (HTHP) polyester dyeing, leveling agents retard the initial dye exhaustion, allowing more time for dye molecules to migrate and achieve uniform coloration. This is especially critical for deep shades and complex color combinations.
The dye bath pH directly impacts the stability of disperse dyes and the dyeing rate. Acetic acid and ammonium sulfate are commonly used to maintain a slightly acidic pH (4.5–5.5), which is optimal for most disperse dye systems. pH buffers prevent sudden shifts during the heating cycle, protecting dye stability and ensuring consistent results across production batches.
After dyeing, unfixed surface dye must be removed to achieve high wash and rub fastness. Reduction clearing with sodium hydrosulfite (sodium dithionite) and caustic soda effectively removes surface deposits of disperse dye, particularly critical for dark shades on polyester. Modern eco-friendly reduction clearing agents have been developed to minimize chemical waste and improve environmental compliance.
For dyeing polyester at atmospheric pressure, carrier auxiliaries are used to swell the fiber and facilitate dye penetration at lower temperatures. However, due to environmental and health concerns, carriers have largely been replaced by HTHP dyeing processes in industrial applications. High-temperature assistants now serve to stabilize the dye bath and protect fiber integrity during prolonged high-temperature processing.
Research consistently demonstrates that optimizing the auxiliary system can improve dye exhaustion rates by 15–30%, reduce dye consumption by up to 20%, and significantly improve color fastness ratings — all while lowering energy and water usage. The right auxiliary combination is not a cost; it is a measurable performance investment.
The global disperse dye market is valued at over USD 4 billion and continues to grow steadily, driven by the expanding polyester textile industry — which now accounts for more than 55% of global fiber consumption. Asia-Pacific, particularly China, India, and Bangladesh, dominates both production and consumption of disperse dyes, with China alone producing approximately 70% of the world's disperse dye output.
In commercial practice, disperse dyes combined with optimized auxiliary systems are deployed across a wide range of industrial applications:
Environmental regulations are pushing the industry toward biodegradable dispersing agents, non-toxic leveling agents, and low-effluent dyeing processes. ZDHC (Zero Discharge of Hazardous Chemicals) compliance is now a baseline requirement for major global brands, driving innovation in green auxiliary chemistry.
Supercritical CO₂ dyeing — which uses pressurized carbon dioxide instead of water as the dyeing medium — is emerging as a revolutionary technology for disperse dyes on polyester. This process eliminates wastewater entirely and requires no auxiliaries for dispersion, representing a paradigm shift in sustainable textile dyeing.
Advanced color management software combined with AI algorithms now enables precise dye and auxiliary formulation, reducing trial-and-error in production. Real-time spectrophotometric monitoring of dye baths allows dynamic adjustment of auxiliary dosages, improving first-time-right rates and reducing batch failures.
The development of disperse dyes with built-in UV absorption, antimicrobial properties, and moisture-wicking functionality — enabled by specialized reactive auxiliaries — is opening new markets in performance apparel, medical textiles, and smart fabrics.
Automotive interior textiles — including seat fabrics, headliners, and door panels — must withstand extreme light exposure, temperature cycling, and abrasion. Disperse dyes with ISO light fastness ratings of 6–7 or above, combined with UV-stabilizing auxiliaries and post-treatment fixatives, are essential for meeting OEM specifications from major automotive manufacturers. The auxiliary system must also be compatible with flame-retardant finishes applied to these technical textiles.
High-performance sportswear demands dyes that maintain color brilliance under repeated washing, perspiration exposure, and UV radiation. Disperse dyes on polyester and polyamide, enhanced with perspiration-resistant auxiliaries and softening agents, deliver the vibrant, durable colors required by leading sportswear brands. The dyeing process must also preserve the stretch and moisture management properties of the technical fabric.
The rapid growth of on-demand and customized textile printing has created enormous demand for sublimation-grade disperse dyes. These dyes must exhibit precise sublimation temperature profiles, high color gamut coverage, and excellent wash fastness after transfer. Auxiliary-enhanced ink formulations improve print sharpness, prevent dye migration on the transfer paper, and optimize color yield during the heat transfer process.
As the textile industry accelerates its shift toward recycled polyester from PET bottles and post-consumer waste, new challenges emerge in disperse dyeing. Recycled polyester fibers often have inconsistent crystallinity, residual impurities, and variable surface chemistry that can cause uneven dye uptake. Specialized auxiliary systems — including pre-treatment agents, modified dispersants, and controlled-release leveling agents — are critical for achieving consistent, high-quality dyeing results on rPET substrates.
Optimized auxiliary systems deliver wash fastness ratings of 4–5 and light fastness of 6–7, meeting the most demanding international standards for textile coloration.
Precision auxiliary formulation reduces dyeing cycle times by up to 25%, lowers dye consumption, and minimizes the need for re-dyeing — directly improving production economics.
Modern auxiliary-enhanced disperse dye systems are formulated to comply with REACH, ZDHC, bluesign®, and OEKO-TEX® STANDARD 100 requirements, supporting global brand sustainability commitments.
Buffered, stabilized dye-auxiliary systems ensure consistent color matching across production batches, reducing quality control costs and customer complaints.
Engineered to perform on standard polyester, recycled rPET, microfibers, polyamide, acetate, and blended fabrics — delivering consistent results across diverse substrate types.
From small-batch specialty production to continuous industrial dyeing at 18,000+ tons annual capacity, auxiliary-optimized disperse dye systems scale seamlessly across all production volumes.
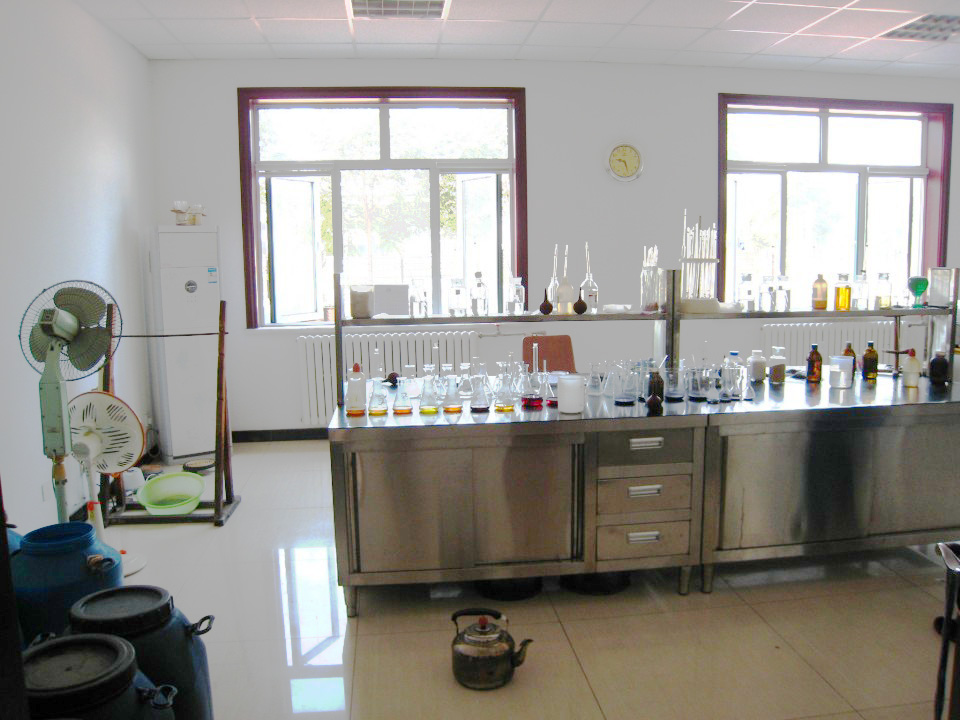
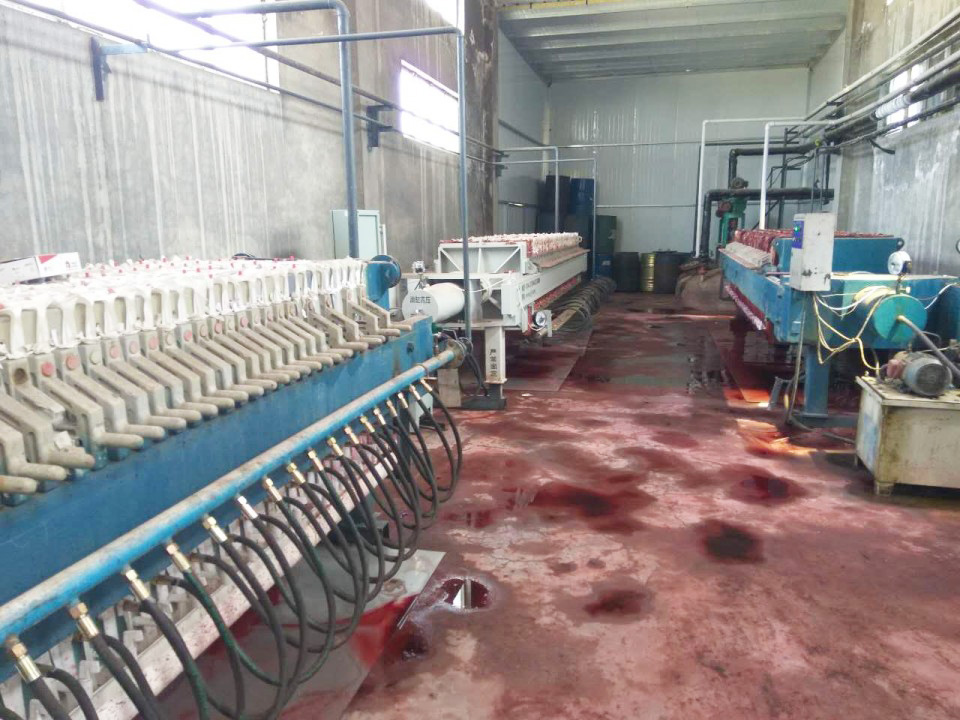
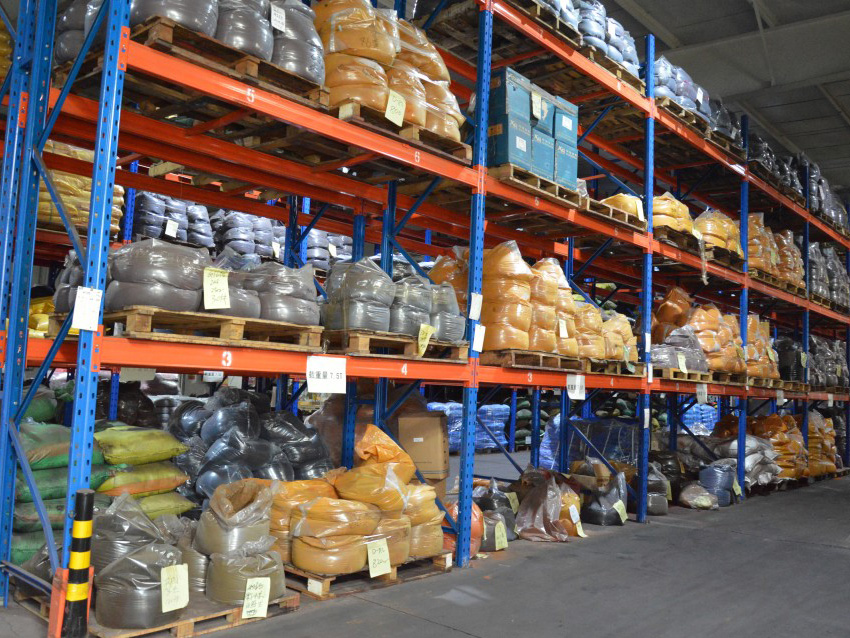
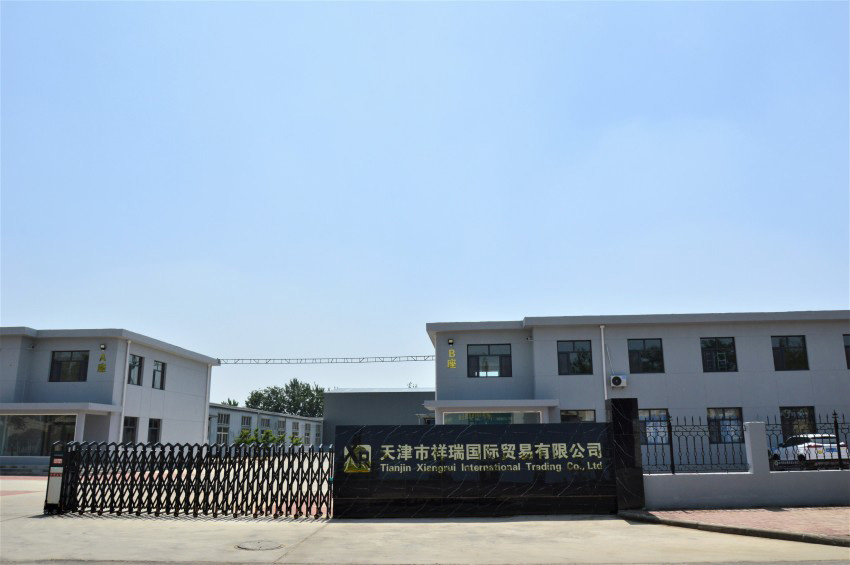
Tianjin Xiangrui Dyestuff Co., Ltd., together with its subsidiary Tianjin Xiangrui International Trading Co., Ltd., was established in 1998 and 2021 respectively. The company is located in Dasi Industrial Park, Xiqing Economic Development Area, Tianjin, China, and currently employs several hundred staff members.
Xiangrui specializes in the manufacture and supply of a wide range of different dyes, pigments, chemical auxiliaries, and intermediates, which are widely applied in industries such as textiles, papermaking, leather, coatings, inks, plastics, rubber, aluminum, cosmetics, and agriculture.
After years of continuous development, Xiangrui has established a fully integrated operation covering research and development, production, sales, and after-sales technical support.
With an annual production capacity of approximately 18,000 tons, Xiangrui is able to provide stable and reliable supply to customers worldwide.
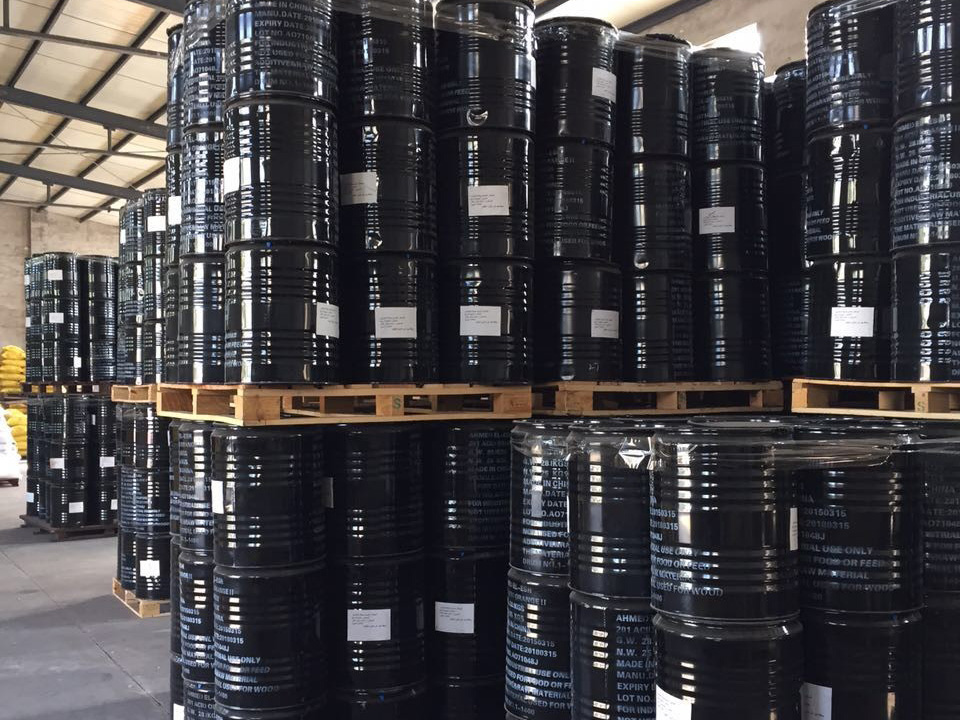
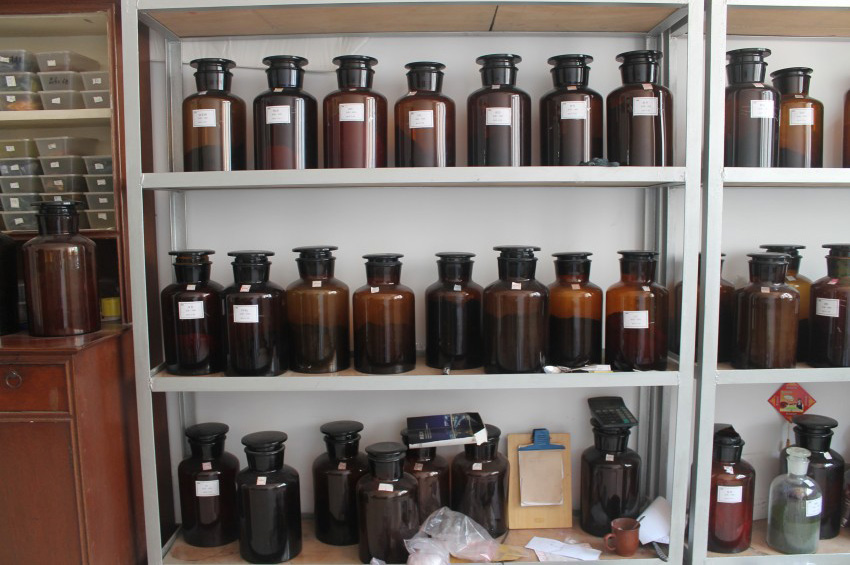
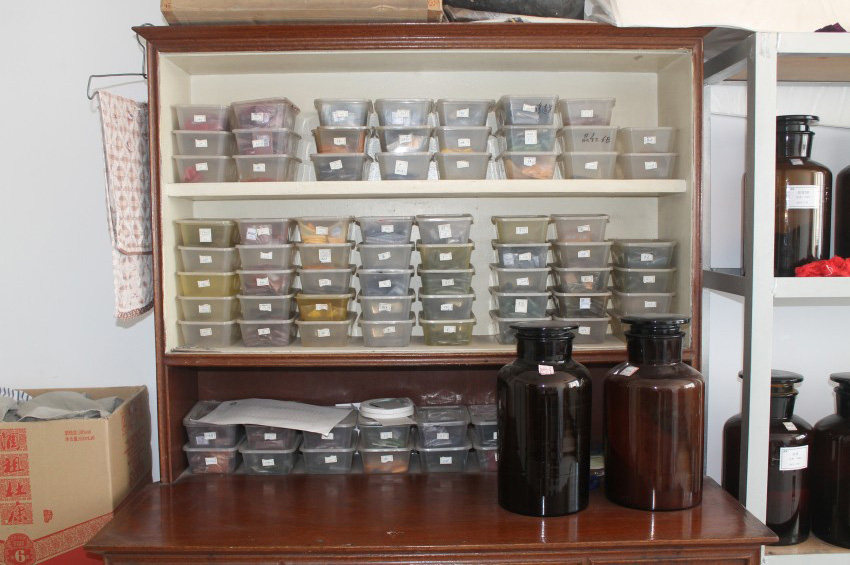
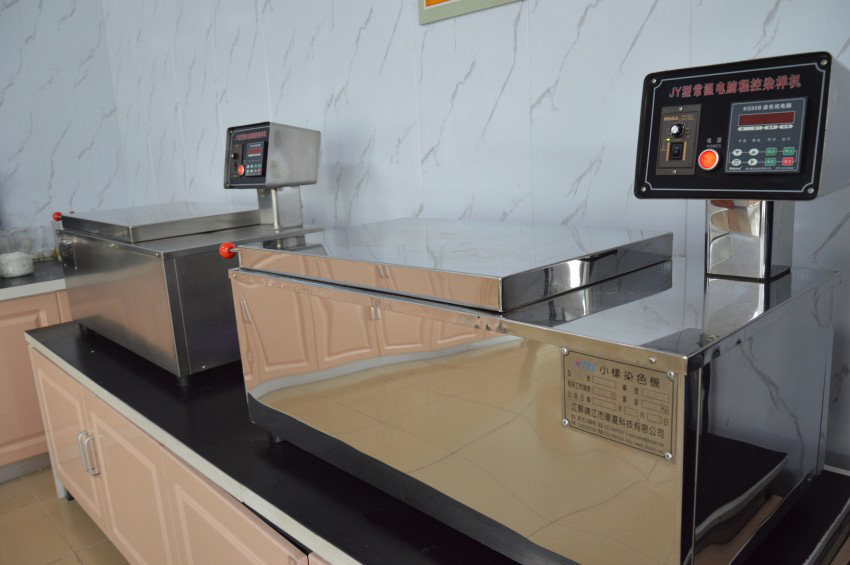
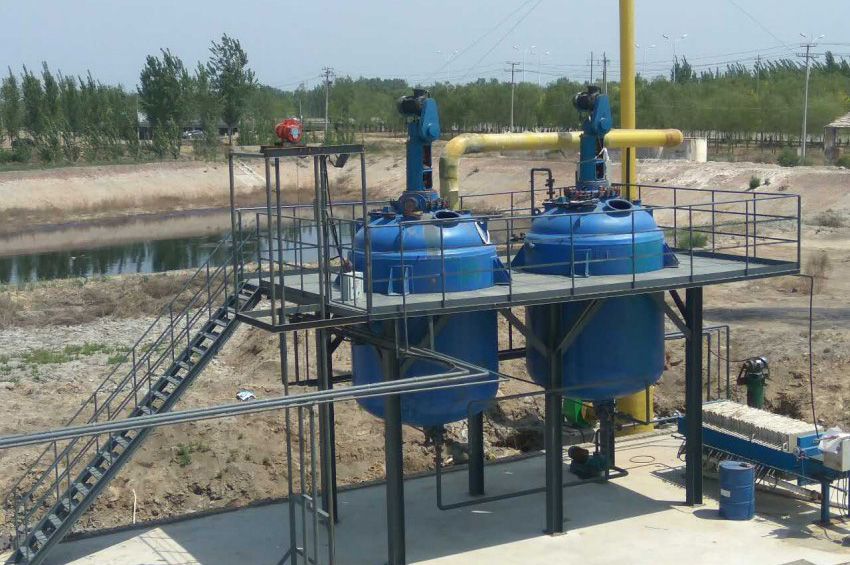
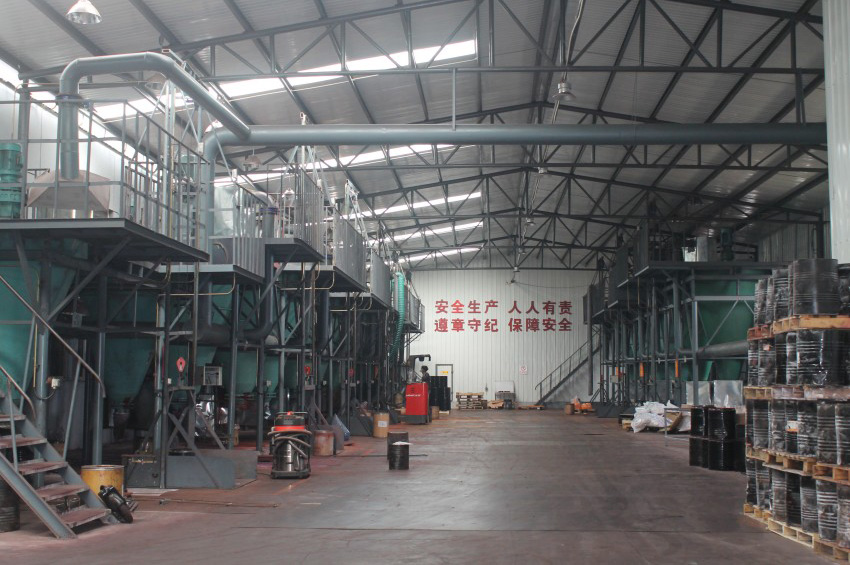
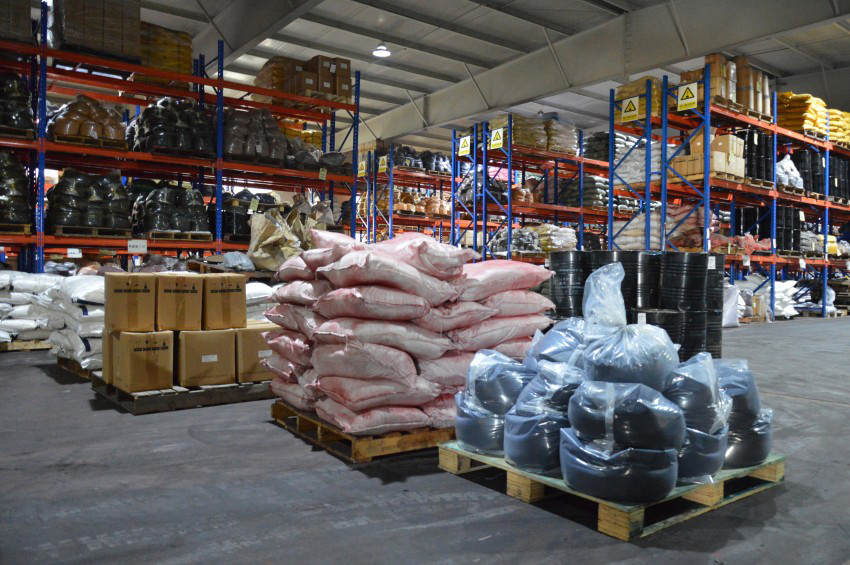
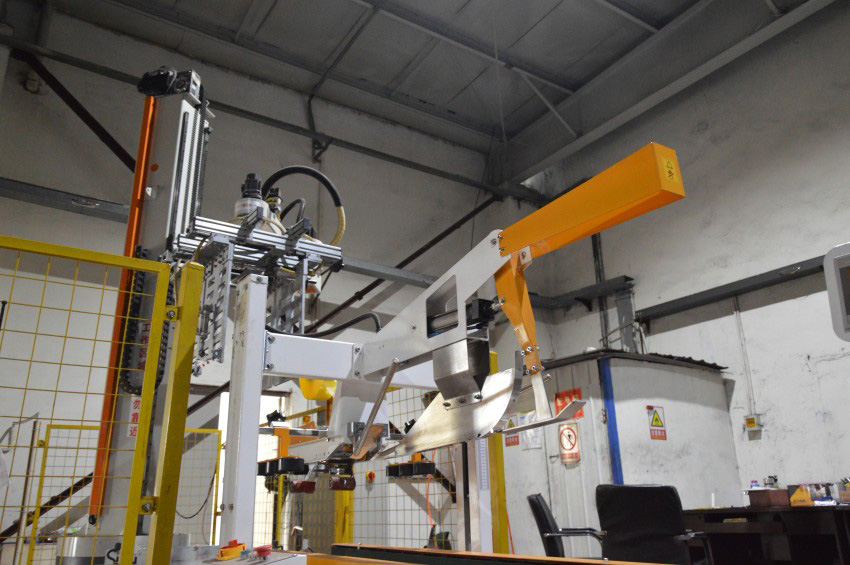
State-of-the-art manufacturing facilities ensuring consistent quality and performance for every batch of disperse dye produced.
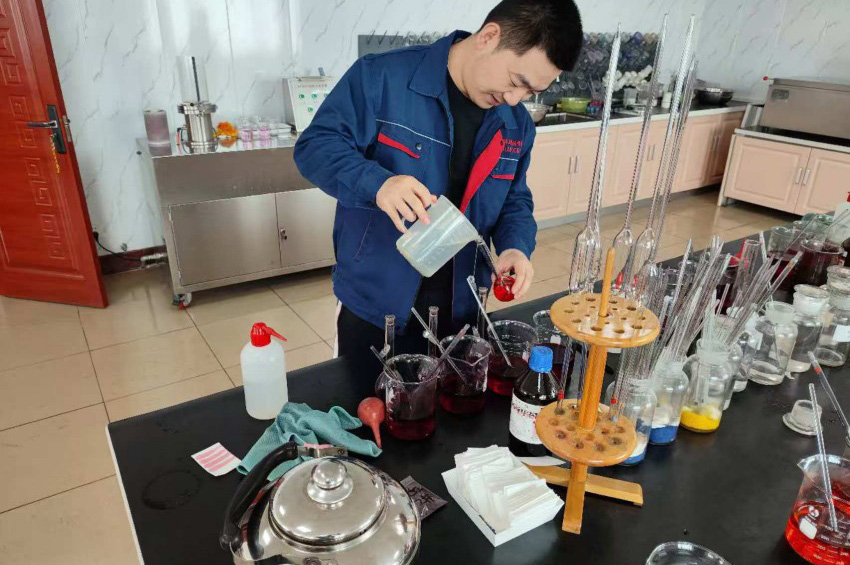
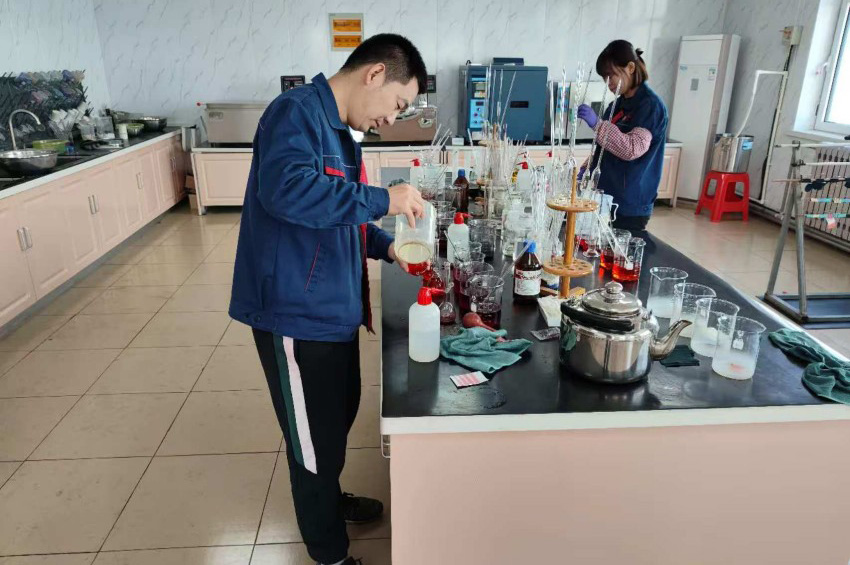
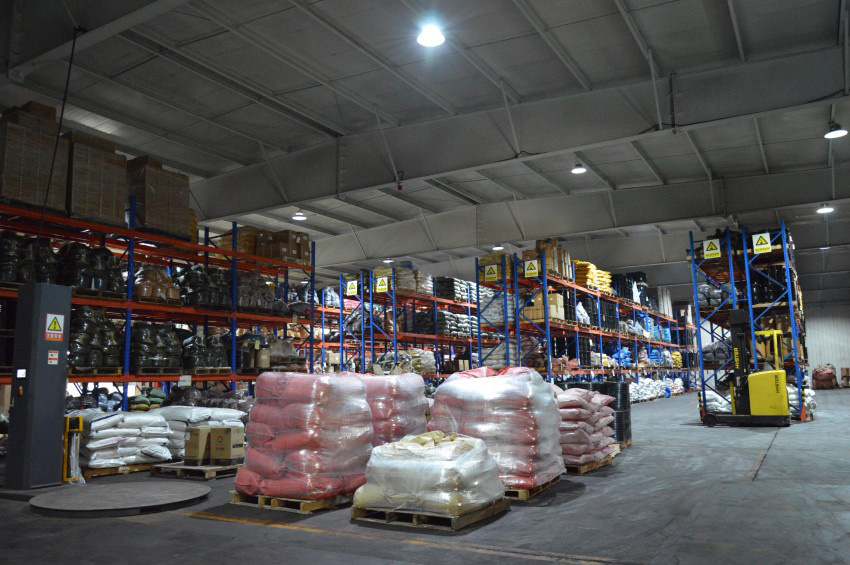
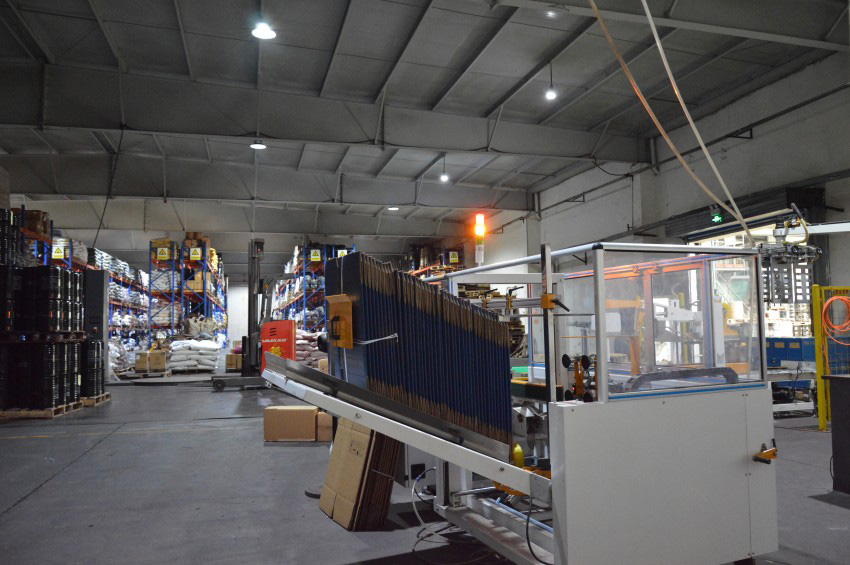
Continuously evaluating gaps from multiple perspectives in order to achieve our goals and improve standardization and management efficiency.
Focusing on strengthening the company's core capabilities, team development, and professional expertise while maintaining an international vision.
Committed to creating long-term value for customers, employees, partners, and society as a whole.
Pursuing continuous innovation and improvement to enhance product quality and to meet the evolving demands of future markets.
Explore our comprehensive range of disperse dyes and chemical auxiliaries for every industrial dyeing application.