Leave Your Message


🔬 The utilization of Latex Paint Pigment For Coloring Textiles And Fabrics has revolutionized the way the global textile industry approaches dyeing and surface modification. Unlike traditional aqueous dyes that rely on chemical affinity with specific fibers, latex-based pigments utilize a sophisticated polymeric binder system. This advanced formulation allows the pigment particles to physically adhere to the surface of virtually any substrate, including cotton, polyester, nylon, and complex blends. The core mechanism involves the coalescence of latex particles during the curing process, forming a continuous, flexible, and highly durable film that encapsulates the colorant. This technological leap not only ensures exceptional color vibrancy and opacity but also significantly enhances the fabric's resistance to mechanical abrasion, UV degradation, and repeated laundering cycles. Furthermore, the modern commercial landscape of textile manufacturing is increasingly demanding solutions that bridge the gap between aesthetic excellence and functional performance, a niche perfectly filled by high-grade latex paint pigments.
In the current industrial context, the transition towards latex paint pigments is heavily driven by stringent environmental regulations and the urgent need for sustainable manufacturing practices. Traditional dyeing processes are notoriously water-intensive, often generating massive volumes of toxic effluent heavily laden with unfixed dyes, heavy metals, and harsh chemical auxiliaries. In stark contrast, latex pigment coloring systems operate on a significantly more eco-friendly paradigm. They typically require zero or minimal water for washing off post-application, thereby drastically reducing water consumption and wastewater treatment burdens. The current formulations are meticulously engineered to be free from volatile organic compounds (VOCs), alkylphenol ethoxylates (APEOs), and formaldehyde, ensuring full compliance with international ecological standards such as OEKO-TEX Standard 100, REACH, and the Zero Discharge of Hazardous Chemicals (ZDHC) guidelines. This profound shift is not merely a regulatory compliance strategy; it represents a fundamental evolution in corporate responsibility and environmental stewardship within the global supply chain.
📈 Analyzing the future development trends, the market for Latex Paint Pigment For Coloring Textiles And Fabrics is poised for exponential growth, characterized by a projected robust Compound Annual Growth Rate (CAGR) over the next decade. One of the most critical drivers of this growth is the advent of smart and functional textiles. Researchers and manufacturers are actively developing multifunctional latex pigments that do more than just impart color. These next-generation pigments are being embedded with nanotechnology to offer advanced functionalities such as antimicrobial properties, flame retardancy, thermal regulation, and even electrical conductivity for wearable electronics. The binder systems are being refined using artificial intelligence and machine learning algorithms to predict polymer behavior, optimize cross-linking density, and achieve the perfect balance between film toughness and the fabric's natural 'hand' or tactile feel. AI-assisted quality control systems utilizing computer vision and spectrophotometry are now standard in state-of-the-art facilities, ensuring absolute color consistency across massive production batches with zero human error.
Delving deeper into specific application scenarios, the versatility of latex paint pigments is truly unmatched. In the realm of Fashion and Apparel, designers are leveraging these pigments for cutting-edge printing techniques, including high-definition digital direct-to-garment (DTG) printing and intricate screen printing. The ability of latex pigments to deliver sharp, photographic-quality prints with unparalleled wash fastness makes them indispensable for modern streetwear and haute couture alike. For Home Textiles and Upholstery, such as curtains, sofa covers, and outdoor furniture fabrics, the paramount requirements are extreme lightfastness and rub resistance. Latex pigments excel in these environments, maintaining their brilliant hues even under prolonged exposure to harsh sunlight and physical friction. Furthermore, in the highly demanding sector of Industrial and Technical Fabrics—which encompasses automotive interiors, military gear, architectural membranes, and geotextiles—latex paint pigments provide vital protective coatings. They enhance the structural integrity of the base fabric while offering customized visual identification, proving that aesthetics and heavy-duty performance can seamlessly coexist.
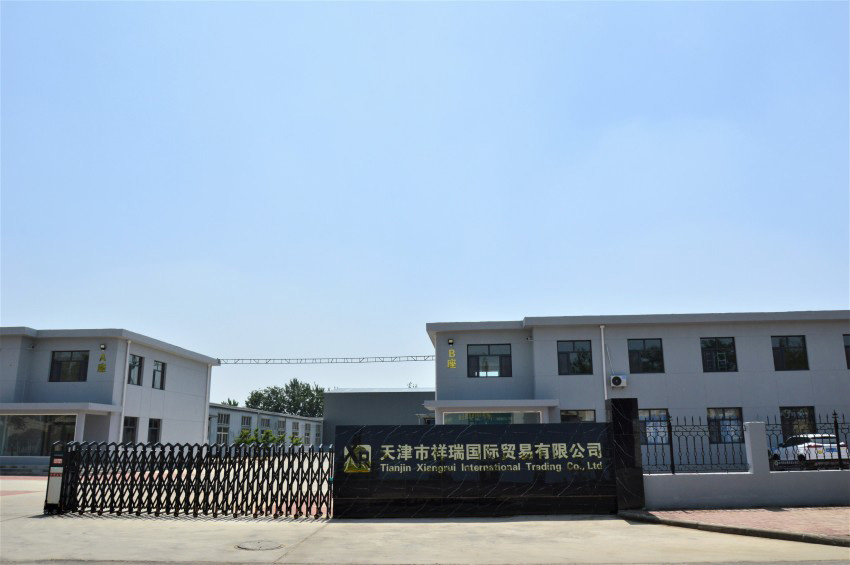
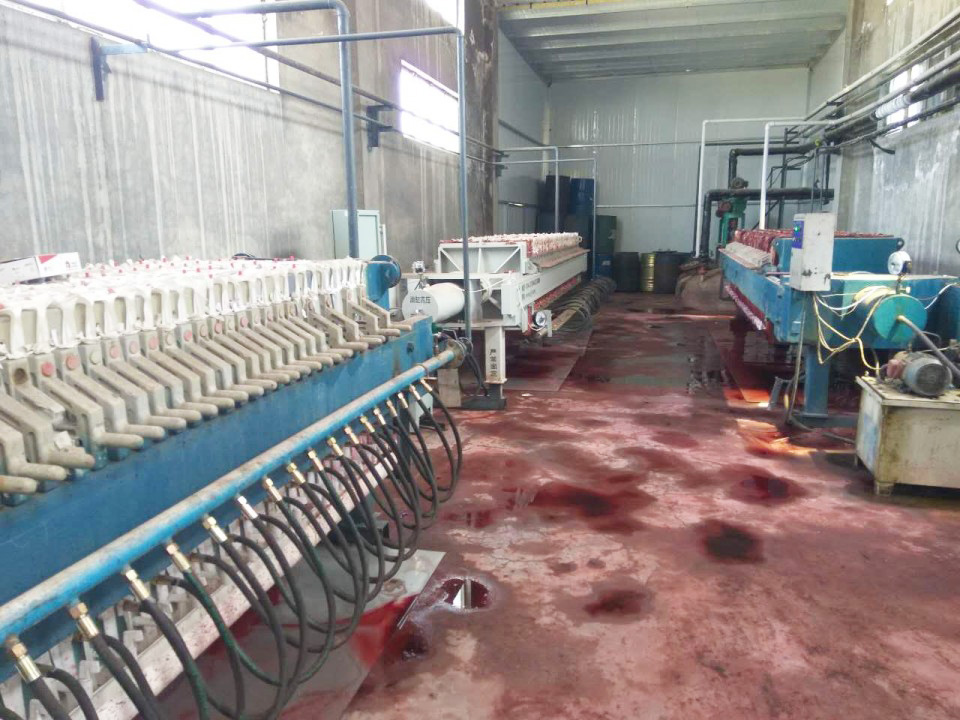
Tianjin Xiangrui Dyestuff Co., Ltd., together with its subsidiary Tianjin Xiangrui International Trading Co., Ltd., was established in 1998 and 2021 respectively. The company is located in Dasi Industrial Park, Xiqing Economic Development Area, Tianjin, China, and currently employs several hundred staff members.
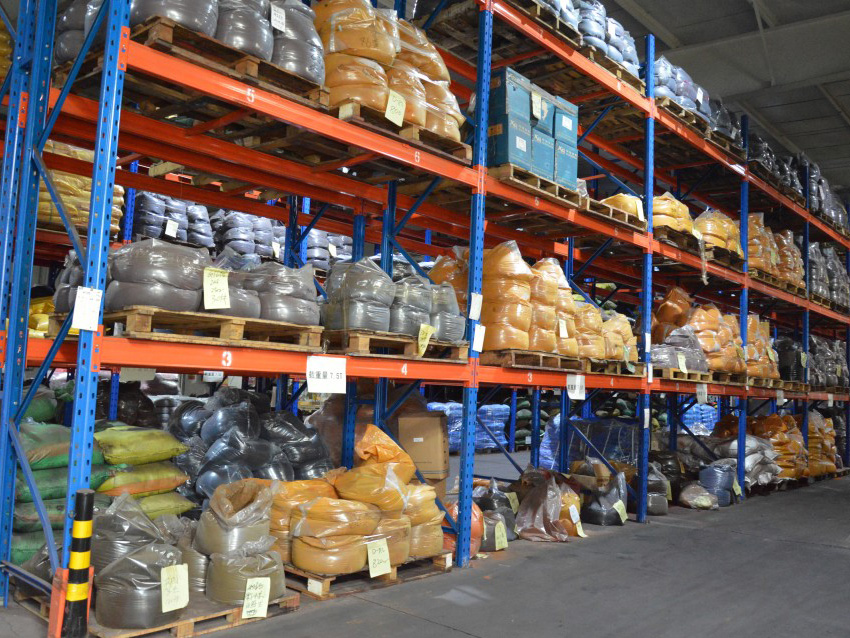
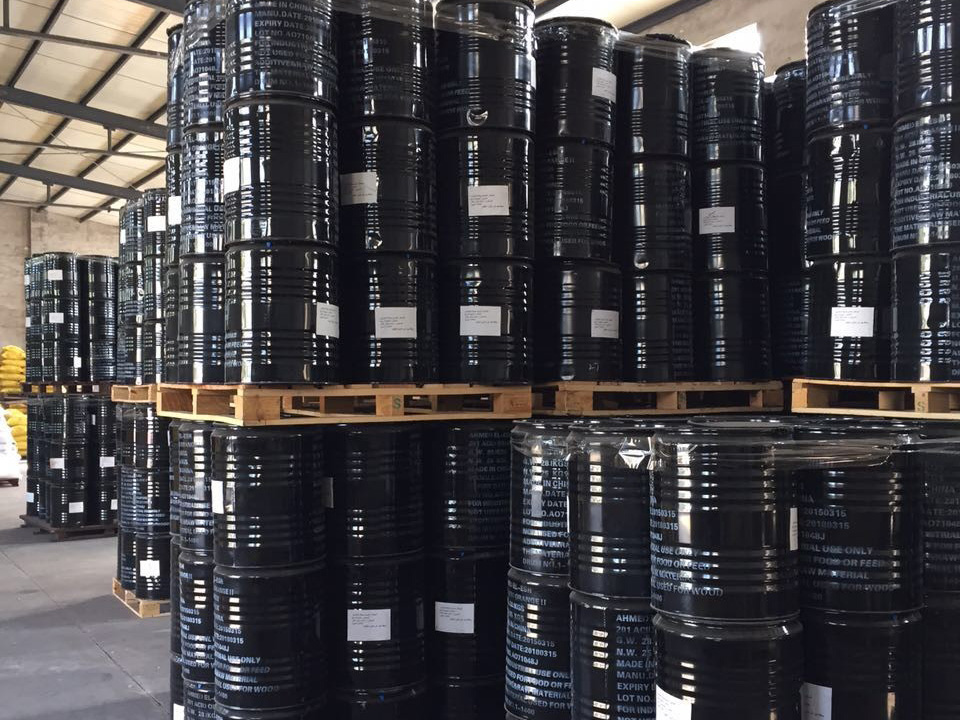
With an annual production capacity of approximately 18,000 tons, Xiangrui is able to provide stable and reliable supply to customers worldwide.
Xiangrui specializes in the manufacture and supply of a wide range of different dyes, pigments, chemical auxiliaries, and intermediates, which are widely applied in multiple industries. We are committed to delivering products with consistent quality and performance for various applications, including the advanced Latex Paint Pigment For Coloring Textiles And Fabrics.
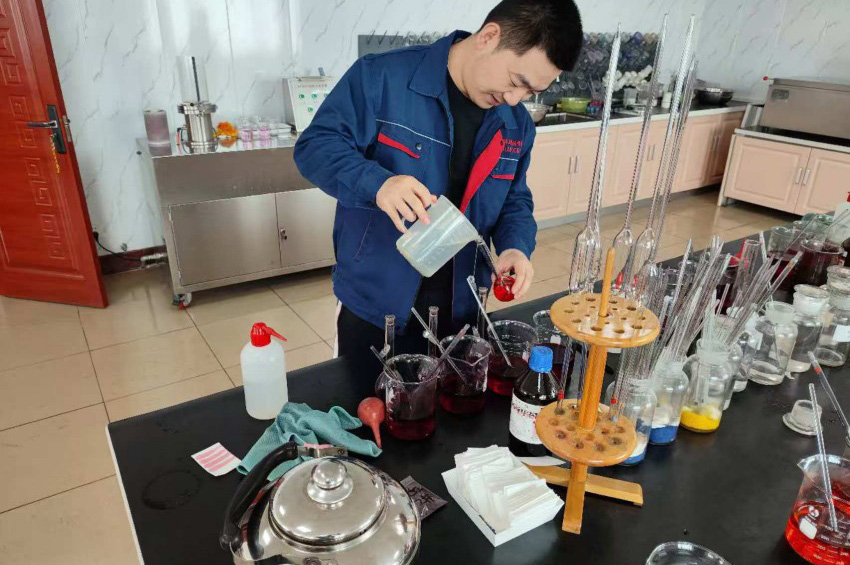
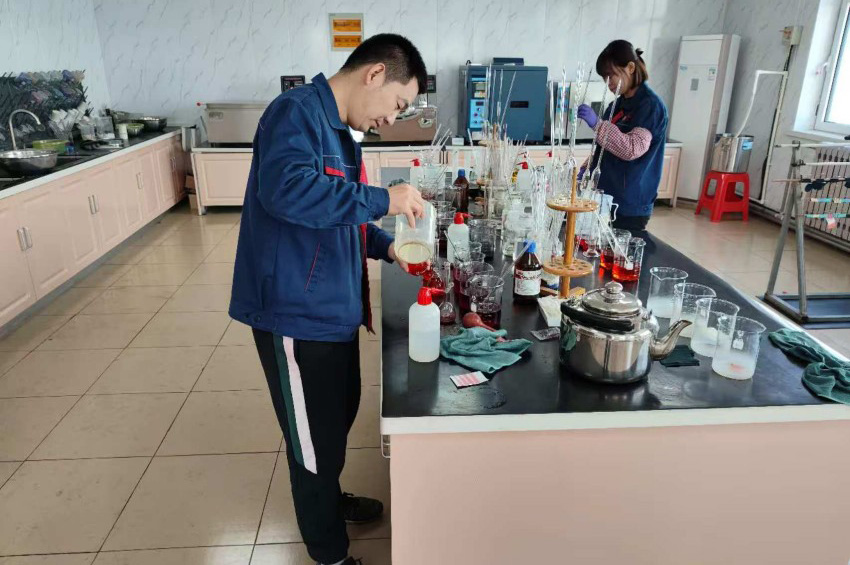
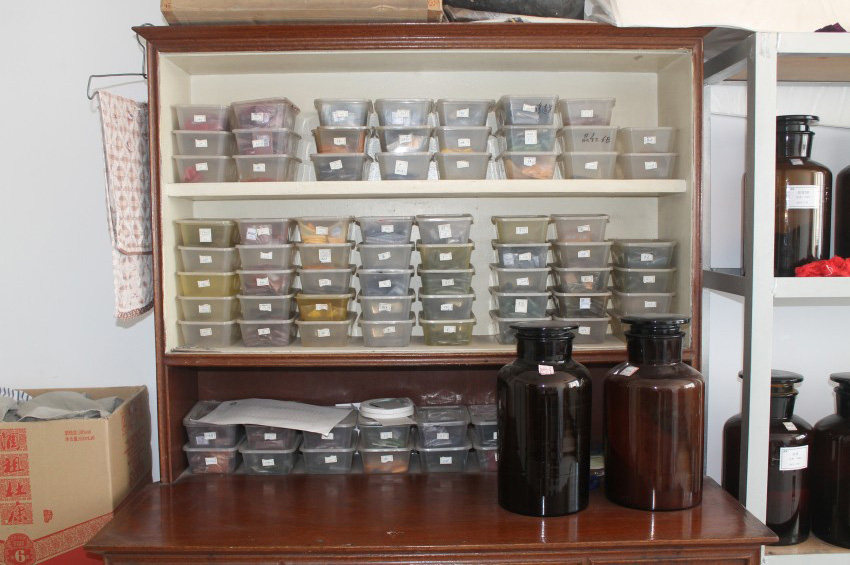
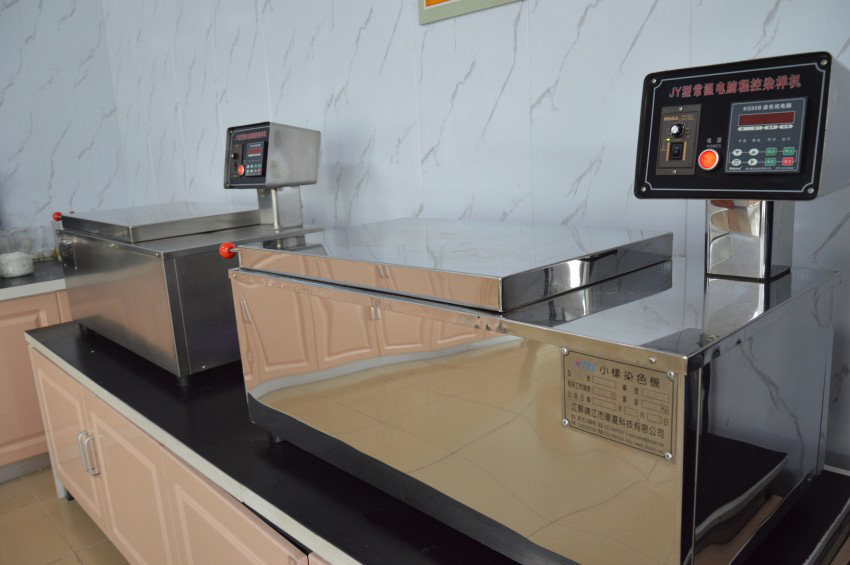
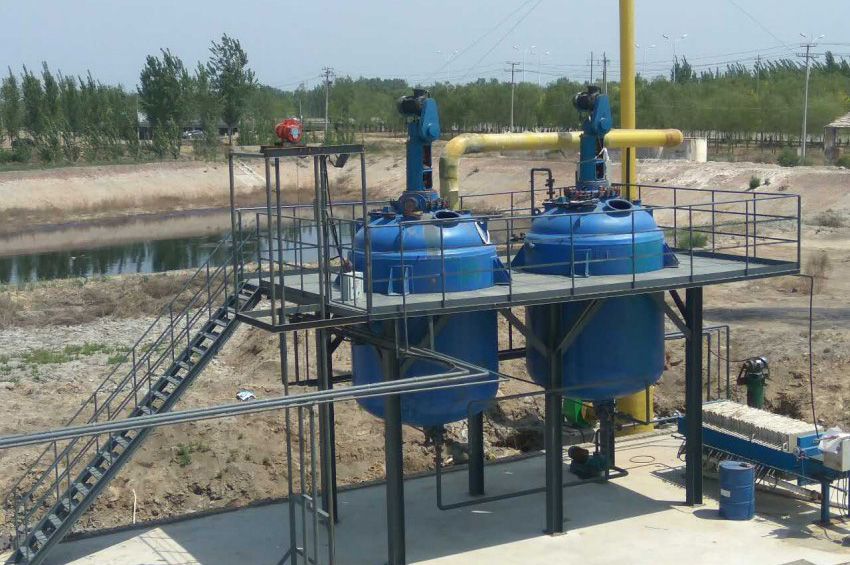
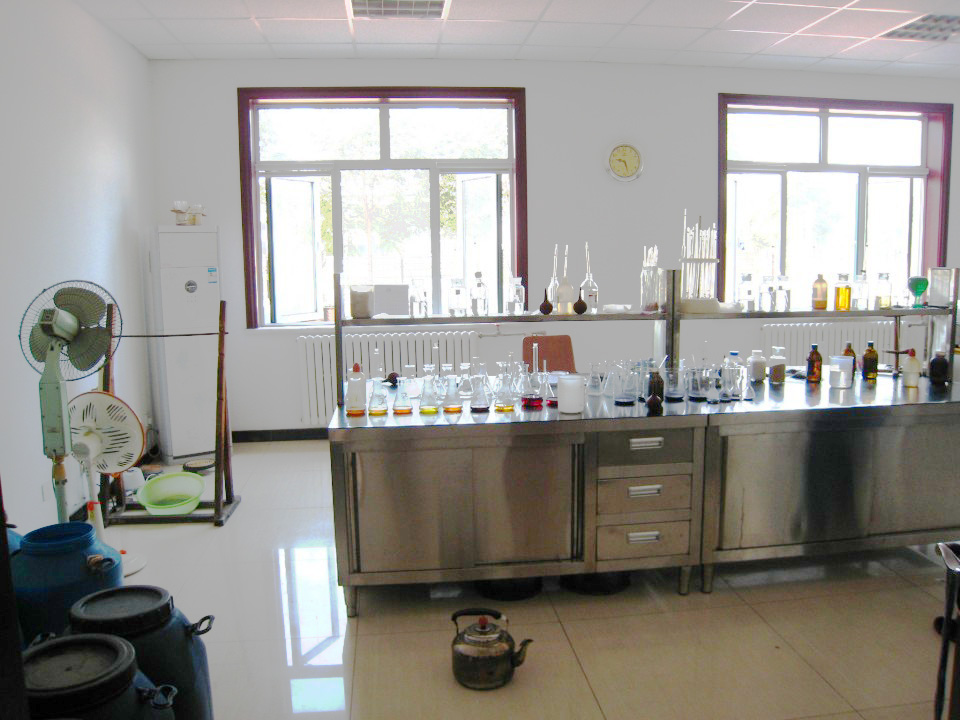
After years of continuous development, Xiangrui has established a fully integrated operation covering research and development, production, sales, and after-sales technical support. Supported by advanced manufacturing facilities, experienced R&D professionals, and a strict quality control system. Owing to superior product quality, professional service, and competitive pricing, Xiangrui has grown into one of the leading dyestuff manufacturers in North China, with products well recognized both in the domestic market and in overseas markets.
Continuously evaluating gaps from multiple perspectives in order to achieve our goals and improve standardization and management efficiency.
Focusing on strengthening the company’s core capabilities, team development, and professional expertise while maintaining an international vision.
Committed to creating long-term value for customers, employees, partners, and society as a whole.
Pursuing continuous innovation and improvement to enhance product quality and to meet the evolving demands of future markets.
With an elite international sales team, experienced technical experts, and a professional quality management system, Xiangrui enjoys a solid reputation among global customers. We strictly implement internal enterprise standards and continuously optimize our management system to meet international market requirements.