


Leave Your Message


High-Performance Textile Auxiliaries for Efficient & Eco-Friendly Dye Processing
Textile Auxiliaries
Direct Fast Dye Direct Blue 199 — High Fastness Textile Dye Solution
Direct Dye
Water Soluble Textile Dye — Direct Fast Brown GTL / Direct Brown 210
Water Soluble DyeChina Textile Auxiliaries Supplier: Enhance Efficiency & Eco-Friendliness at Our Factory
Eco-Friendly AuxiliariesTextile dyes are chemical compounds that impart color to fibers, yarns, and fabrics through chemical or physical bonding. From reactive dyes for cotton to disperse dyes for polyester, the diversity of dye chemistry reflects the vast complexity of modern textile manufacturing. However, the performance of any dye system is rarely determined by the dye molecule alone.
This is where textile auxiliaries become indispensable. Auxiliaries — including leveling agents, fixing agents, softeners, wetting agents, dispersants, and anti-foaming agents — act as functional enablers that dramatically improve dye uptake, color uniformity, fastness ratings, and process reproducibility. Without the right auxiliary formulation, even the most advanced dye can underperform.
The global textile dye market, valued at over USD 9 billion, is being reshaped by tightening environmental regulations, rising consumer expectations for sustainability, and the accelerating digital transformation of dyehouses. In this landscape, the synergy between high-quality dyes and precision-engineered auxiliaries is not merely a technical preference — it is a competitive necessity.
Modern dye performance is a system-level outcome. Auxiliaries control the kinetics of dye diffusion, regulate bath pH, prevent aggregation, and lock color into fiber structures. Selecting the correct auxiliary combination can increase dye exhaustion rates by 15–30%, reduce water and energy consumption, and elevate color fastness by one to two grades — translating directly into cost savings and quality premiums for textile manufacturers.
The industrial dyeing sector is undergoing a profound transformation. Understanding the commercial forces at play is essential for manufacturers, buyers, and formulators seeking competitive advantage.
The global textile dye and auxiliary market continues to expand, driven by rising apparel demand in Asia-Pacific and Africa. China remains the world's largest producer and exporter of textile dyes, supplying over 60% of global reactive dye volumes. Auxiliaries represent a rapidly growing segment, with CAGR projections of 5–7% through 2030, as dyehouses invest in process optimization chemicals.
REACH regulations in Europe, ZDHC (Zero Discharge of Hazardous Chemicals) standards, and OEKO-TEX certification requirements are forcing manufacturers to reformulate both dyes and auxiliaries. Low-salt, low-alkali reactive dyeing systems paired with eco-compatible auxiliaries are now a market prerequisite for supplying major fashion brands and retailers.
Energy, water, and chemical costs account for 30–45% of total dyehouse operating expenses. Auxiliaries that improve first-time-right (FTR) dyeing rates, reduce re-dyeing, and enable lower-temperature processing offer measurable ROI. Manufacturers adopting integrated dye-auxiliary systems report 20–35% reductions in overall process costs versus conventional approaches.
Smart dyeing systems equipped with IoT sensors, AI-driven recipe management, and automated dosing are creating new demand for precisely characterized auxiliaries. Dye auxiliaries must now meet tighter consistency standards to function reliably in automated dispensing environments, pushing suppliers toward ISO-certified, batch-traceable formulations.
Bio-based auxiliaries, waterless dyeing enablers, and biodegradable surfactant systems are transitioning from niche to mainstream. Brands including H&M, Inditex, and Patagonia now mandate supplier compliance with sustainable chemistry frameworks, creating strong commercial pull for next-generation dye-auxiliary combinations that minimize ecological footprint.
Leading suppliers are investing heavily in application laboratories where dye-auxiliary interactions are systematically characterized. Proprietary auxiliary blends tailored to specific dye classes — such as optimized leveling agents for reactive dyes or specialized carriers for disperse dyeing — are becoming key differentiators in a commoditizing market.
From fiber preparation to final finishing, auxiliaries intervene at every critical stage of the dyeing process. Here are the key industrial scenarios where their impact is most pronounced.
Reactive dyes achieve covalent bonding with cellulose, but hydrolysis side-reactions reduce fixation efficiency. Alkali-buffer auxiliaries, migration inhibitors, and anti-back-staining agents work in concert to push fixation rates above 80%, reduce salt consumption, and prevent unlevel dyeing — critical for solid-color garment production and denim manufacturing.
High-temperature disperse dyeing (130°C) requires dispersants to maintain dye particle stability under extreme conditions, preventing aggregation and filter press contamination. Auxiliary leveling agents slow dye migration to ensure uniform shade across fabric widths, while reduction-clearing auxiliaries remove surface dye deposits after dyeing — essential for automotive textiles and sportswear.
Acid dyes on nylon and wool require precise pH management and leveling agents to overcome the fiber's non-uniform dye-site distribution. Amphoteric leveling auxiliaries compete with dye molecules for fiber sites, retarding initial uptake and enabling migration to achieve uniform coverage. Anti-felting auxiliaries for wool protect fiber structure during high-agitation dyeing processes.
Direct dyes — including Direct Blue 199 and Direct Brown 210 — are applied across textiles, paper, and leather with auxiliary wetting agents and fixatives that improve exhaustion and wet fastness. In leather dyeing, penetrating auxiliaries ensure even color distribution through thick hides, while fixing agents lock the dye against perspiration and wet rubbing.
Vat dyes deliver exceptional light and wash fastness, making them the standard for workwear, military fabrics, and home textiles. Reducing agents, oxidation auxiliaries, and sequestering agents are critical to the multi-stage vat dyeing process. Proper auxiliary selection prevents bronzing, ensures complete oxidation, and maintains shade consistency across production batches.
After dyeing, softeners, hand-builders, anti-pilling agents, and UV-absorbers applied with auxiliary carriers transform fabric handle and functional performance. Cationic softeners interact with negatively charged dyed fibers to impart silky texture without shade alteration. Optical brightening agents (OBAs) used in conjunction with fluorescent dyes demand compatible auxiliaries to avoid quenching effects.
Scouring & desizing agents remove impurities; wetting agents ensure uniform substrate preparation for dye absorption.
Dispersants, sequestering agents, and pH buffers prepare the bath for stable dye dissolution and controlled exhaustion.
Leveling agents regulate dye uptake rate; migration promoters ensure uniform shade across the entire substrate.
Fixing auxiliaries form covalent or ionic bonds between dye and fiber, maximizing wet and rub fastness ratings.
Soaping agents remove unfixed dye; softeners, UV-protectors, and anti-static agents deliver final functional properties.
The next decade will see textile dyeing transformed by several converging technological and market forces. Waterless and low-water dyeing technologies — including supercritical CO₂ dyeing, foam dyeing, and air-dyeing systems — require entirely new auxiliary formulations designed for non-aqueous or ultra-low-liquor-ratio environments.
Nano-auxiliary systems are emerging as a frontier area, with nano-encapsulated dyes and sub-micron dispersant particles enabling unprecedented penetration depth, shade brilliance, and functional performance in technical textiles. These systems are being piloted in high-value applications including protective clothing, medical textiles, and smart fabrics.
Circular economy integration is driving demand for auxiliaries compatible with closed-loop water recycling systems and enzymatic dye degradation processes. Dyehouses targeting zero liquid discharge (ZLD) require auxiliaries that do not interfere with wastewater treatment membranes or biological treatment stages.
Finally, AI-assisted formulation is accelerating the development of optimized dye-auxiliary combinations. Machine learning models trained on thousands of dyeing trials can now predict the optimal auxiliary blend for any given dye class, substrate, and performance target — compressing development cycles from months to days.
Sustainability mandates, digital manufacturing, performance textile growth, and supply chain regionalization are the four macro forces accelerating innovation in textile dye-auxiliary systems through 2030 and beyond.
Asia-Pacific accounts for over 70% of global textile dye consumption. China, India, Bangladesh, and Vietnam are the primary manufacturing hubs, with growing demand for premium auxiliaries driven by fast-fashion supply chain quality requirements and export compliance standards.
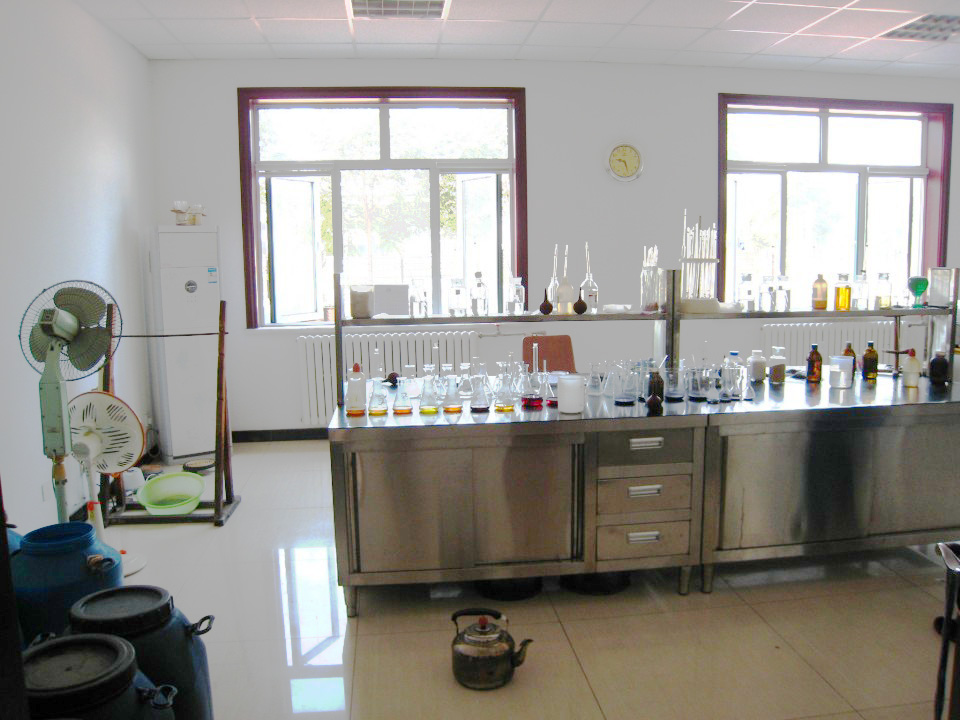
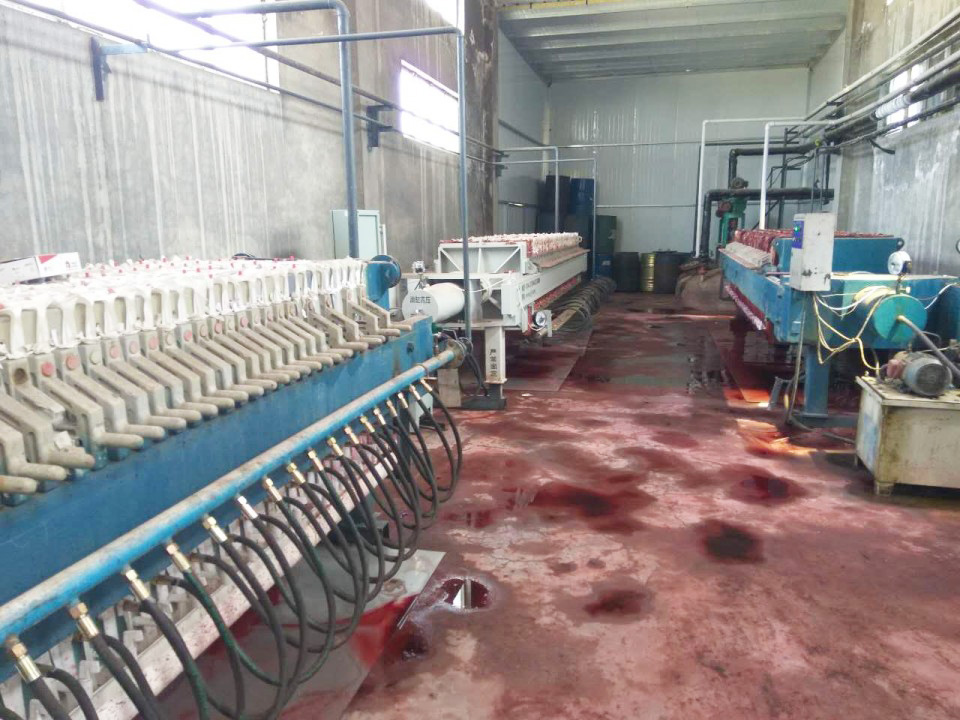
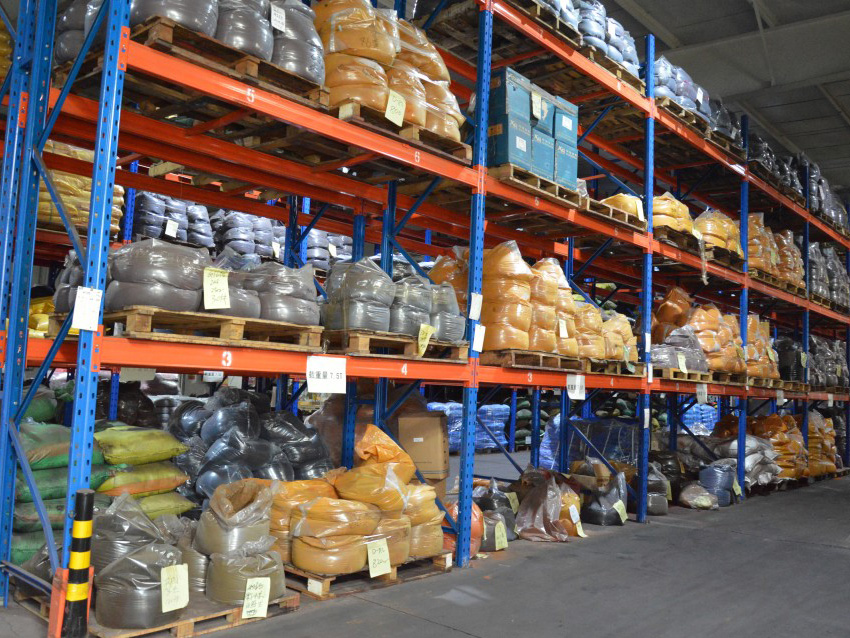
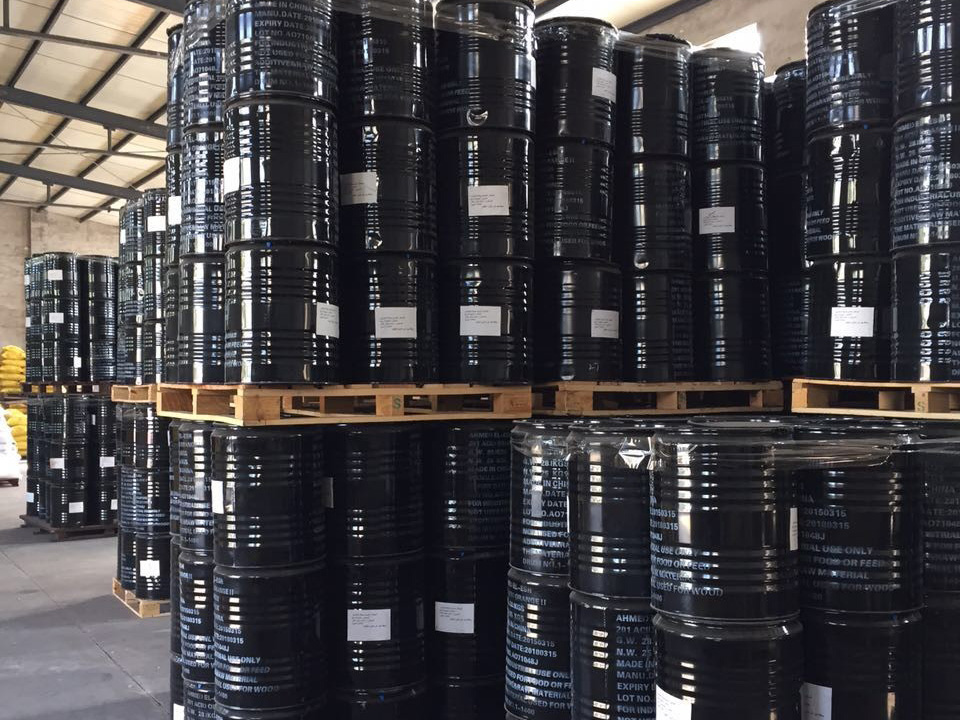
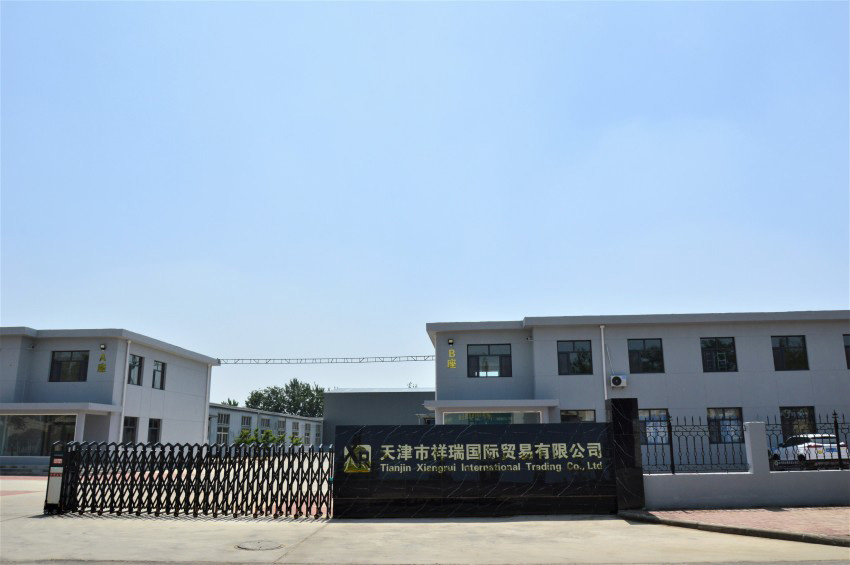
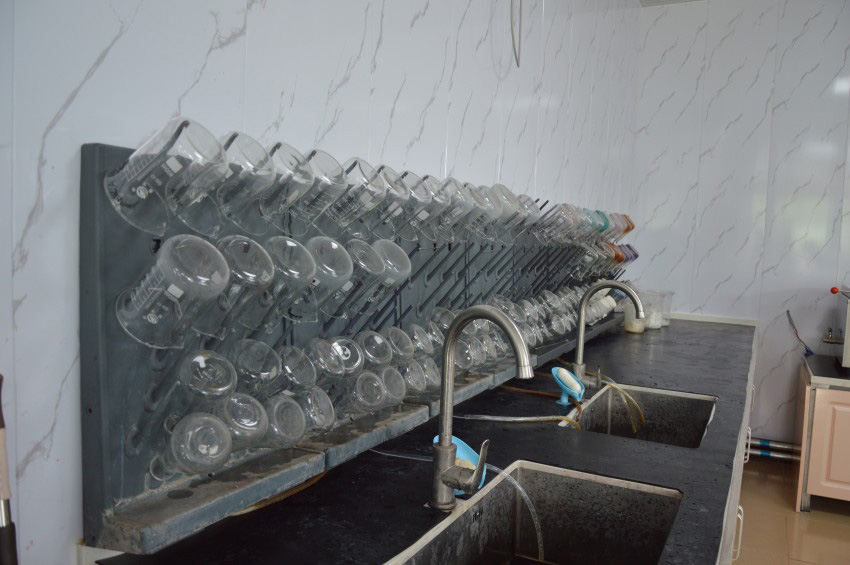
Tianjin Xiangrui Dyestuff Co., Ltd., together with its subsidiary Tianjin Xiangrui International Trading Co., Ltd., was established in 1998 and 2021 respectively. The company is located in Dasi Industrial Park, Xiqing Economic Development Area, Tianjin, China, and currently employs several hundred staff members.
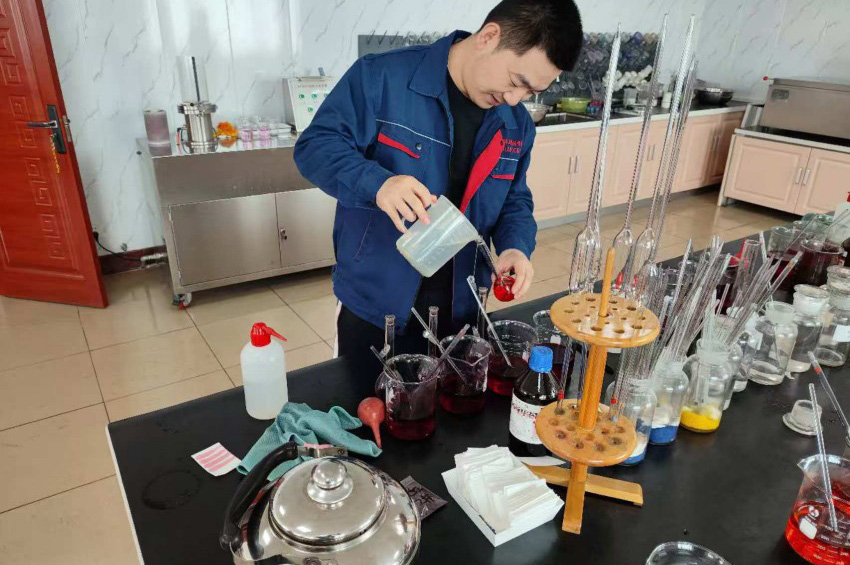
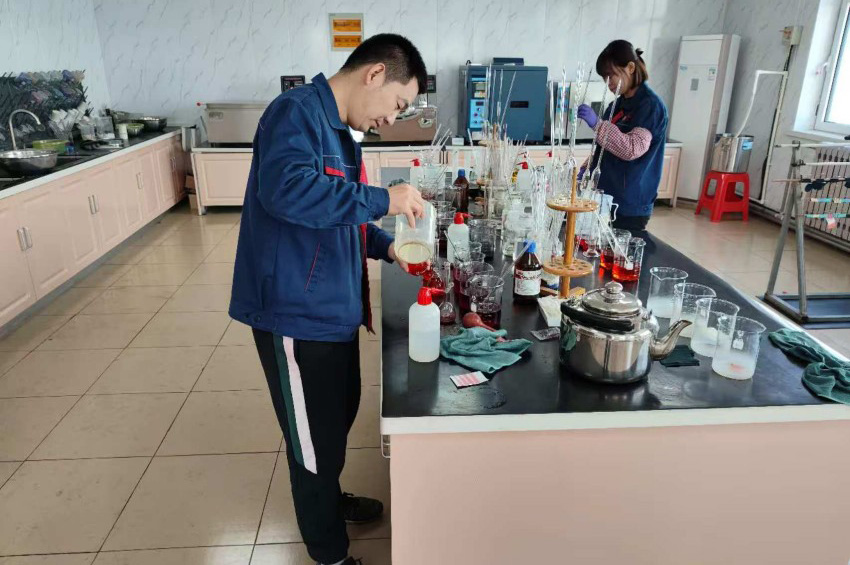
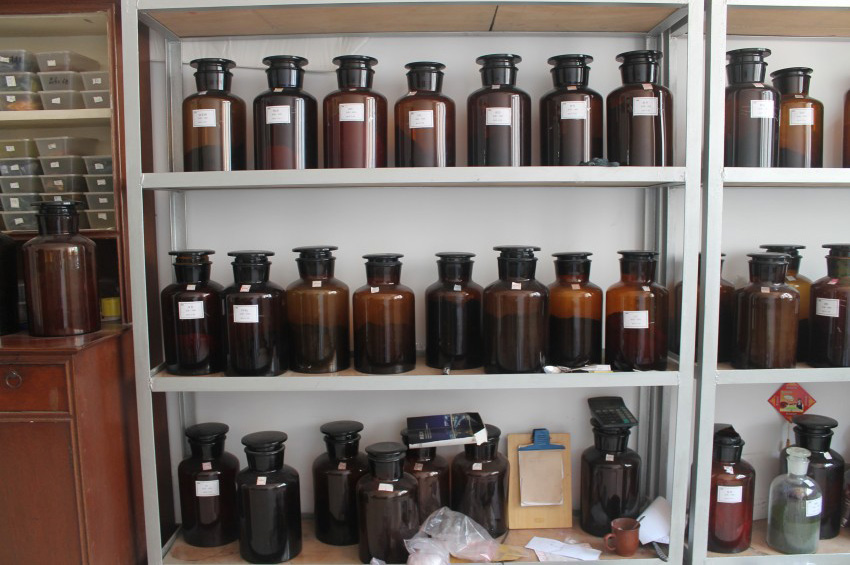
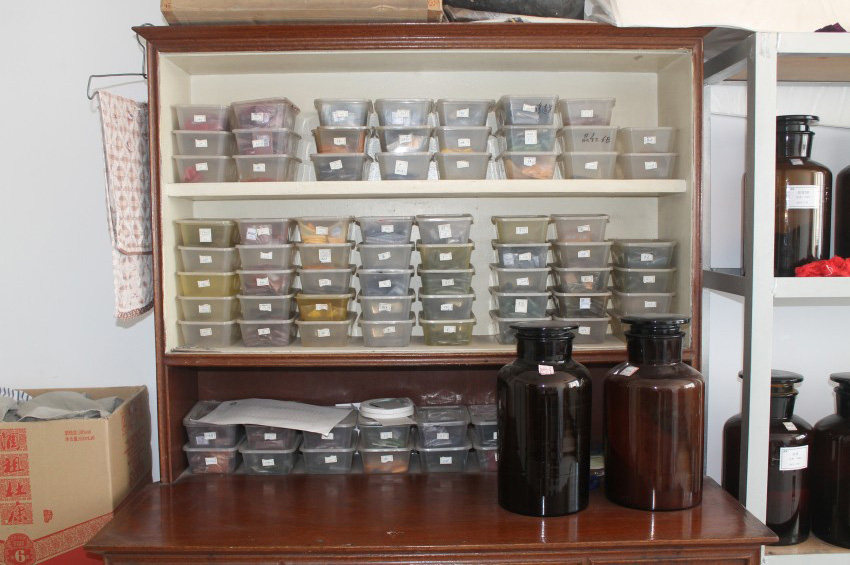
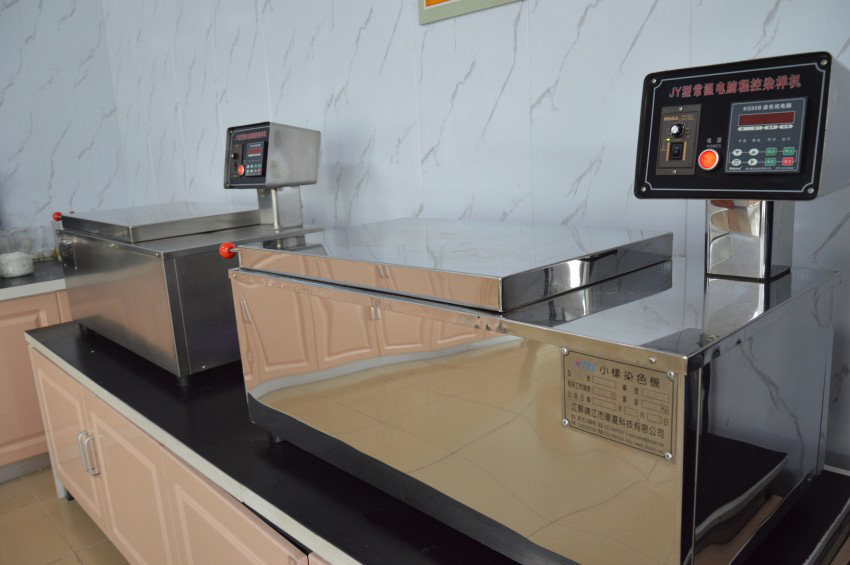
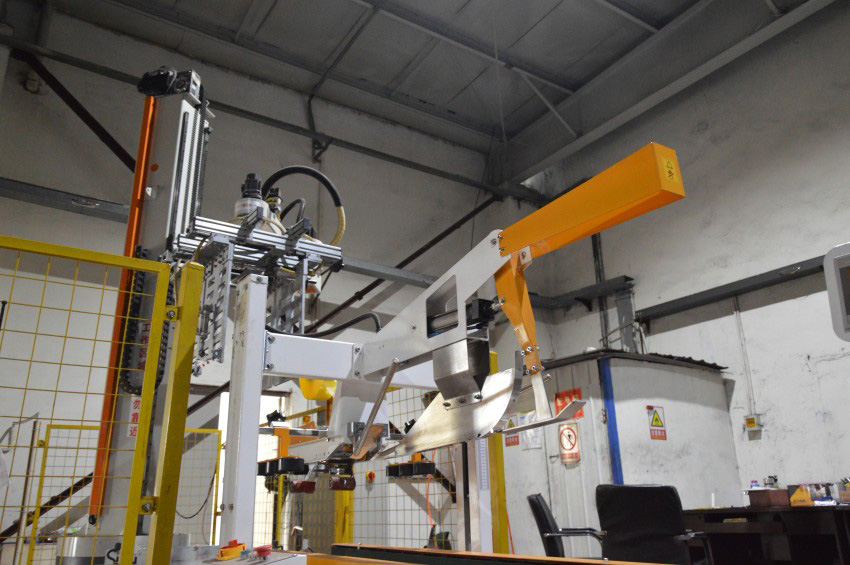
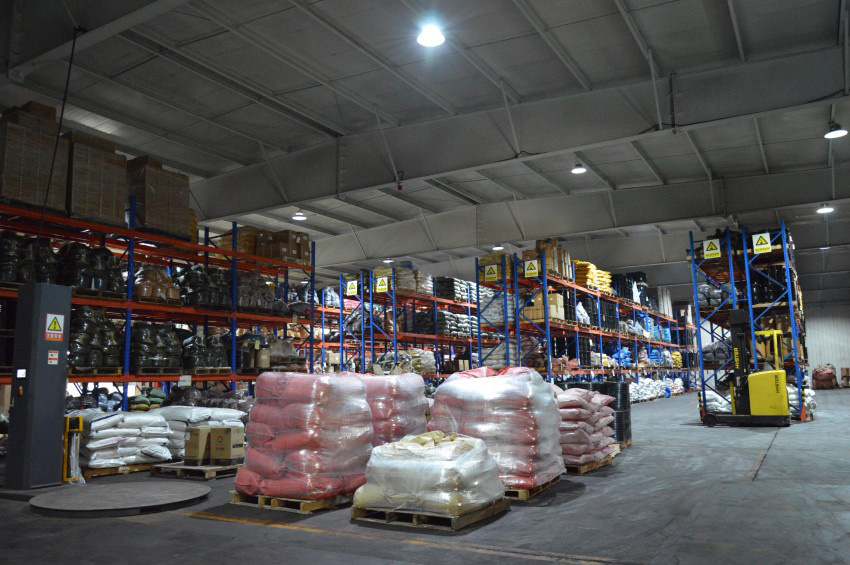
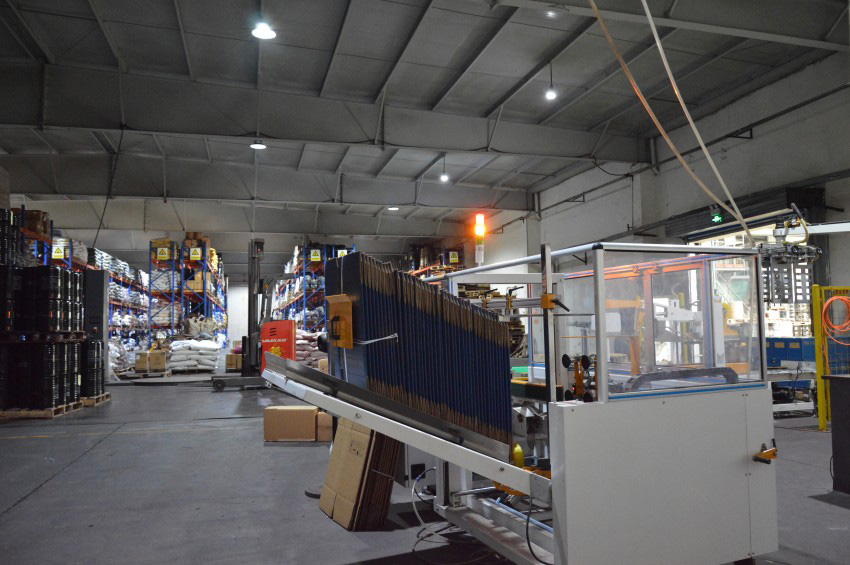
After years of continuous development, Xiangrui has established a fully integrated operation covering research and development, production, sales, and after-sales technical support. Supported by advanced manufacturing facilities, experienced R&D professionals, and a strict quality control system, we are committed to delivering products with consistent quality and performance.
Owing to superior product quality, professional service, and competitive pricing, Xiangrui has grown into one of the leading dyestuff manufacturers in North China, with products well recognized both in the domestic market and in overseas markets.
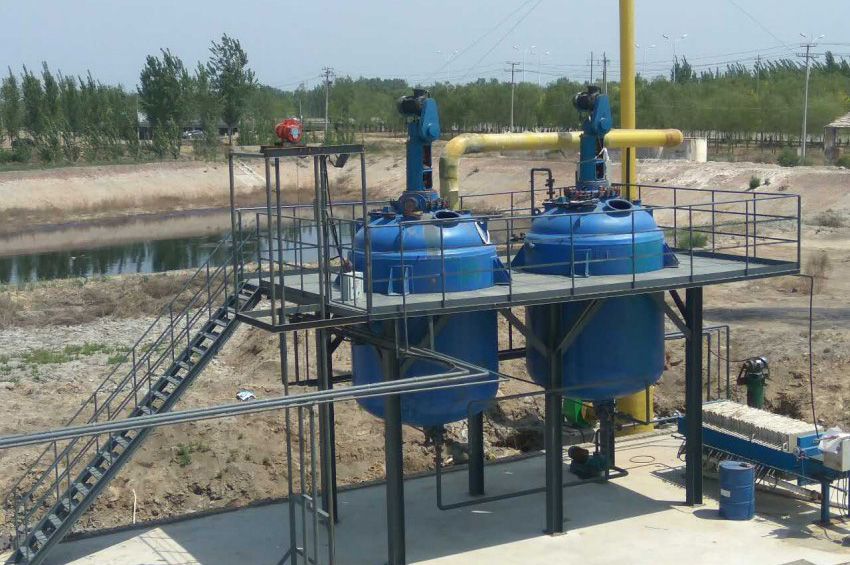
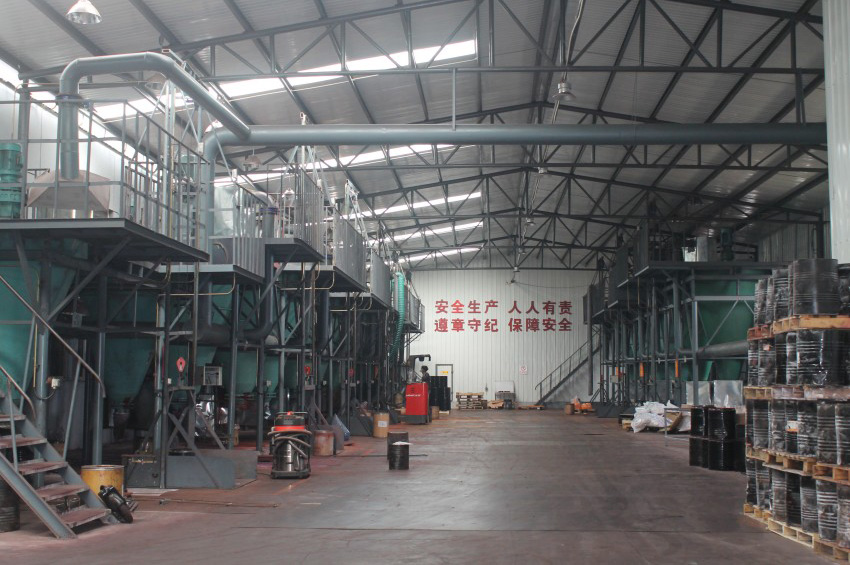
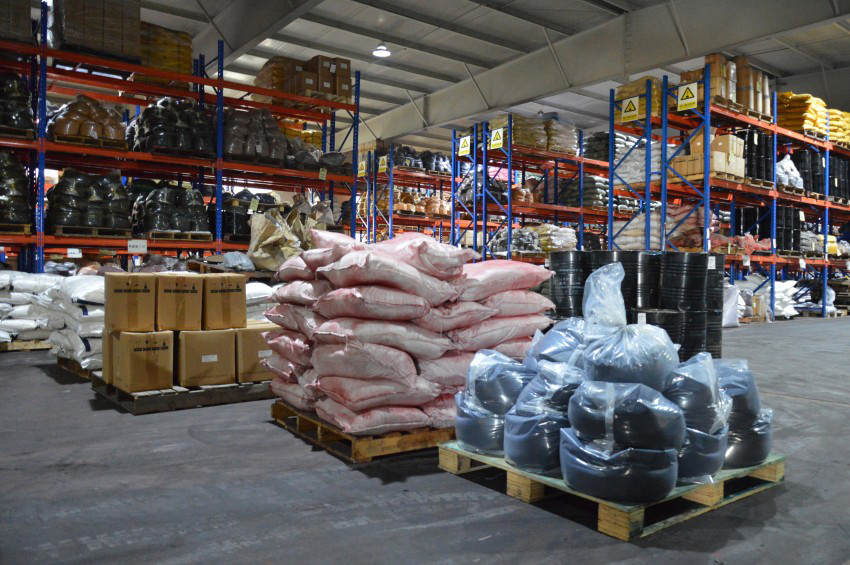
Xiangrui specializes in the manufacture and supply of a wide range of different dyes, pigments, chemical auxiliaries, and intermediates, which are widely applied in industries such as textiles, papermaking, leather, coatings, inks, plastics, rubber, aluminum, cosmetics, and agriculture. With an annual production capacity of approximately 18,000 tons, Xiangrui is able to provide stable and reliable supply to customers worldwide.
Continuously evaluating gaps from multiple perspectives in order to achieve our goals and improve standardization and management efficiency.
Focusing on strengthening the company's core capabilities, team development, and professional expertise while maintaining an international vision.
Committed to creating long-term value for customers, employees, partners, and society as a whole.
Pursuing continuous innovation and improvement to enhance product quality and to meet the evolving demands of future markets.
With an elite international sales team, experienced technical experts, and a professional quality management system, Xiangrui enjoys a solid reputation among global customers. We strictly implement internal enterprise standards and continuously optimize our management system to meet international market requirements.
High-Performance Textile Auxiliaries from China Suppliers and Factory for Efficient and Eco-Friendly Processing
Textile AuxiliariesDirect Fast Dye Direct Blue 199
Direct DyeWater Soluble Dye Direct Fast Brown GTL Direct Brown 210
Water Soluble DyeHigh-Performance Textile Auxiliaries from China Suppliers: Enhance Efficiency and Eco-Friendliness at Our Factory
Eco-FriendlyDye Intermediates Suppliers and Factory in China for Dyes, Pigments, Pharmaceuticals, and More
Dye Intermediates
High Color Fastness Vat Dyes from China Suppliers and Factory for Durable Textile Coloring
Vat DyesDye Intermediates from China: Leading Suppliers and Factory for Dyes and Organic Pigments
Organic Pigments
Textile Direct Dye Direct Blue 6
Direct Dye